
Precision in Every For Critical Engineering
Manufacturing custom, high-tolerance aluminium extrusions with state-of-the-art hydraulic presses, in-house CAD die engineering, and comprehensive surface treatment facilities.
High-volume PLC automated press lines running 24/7
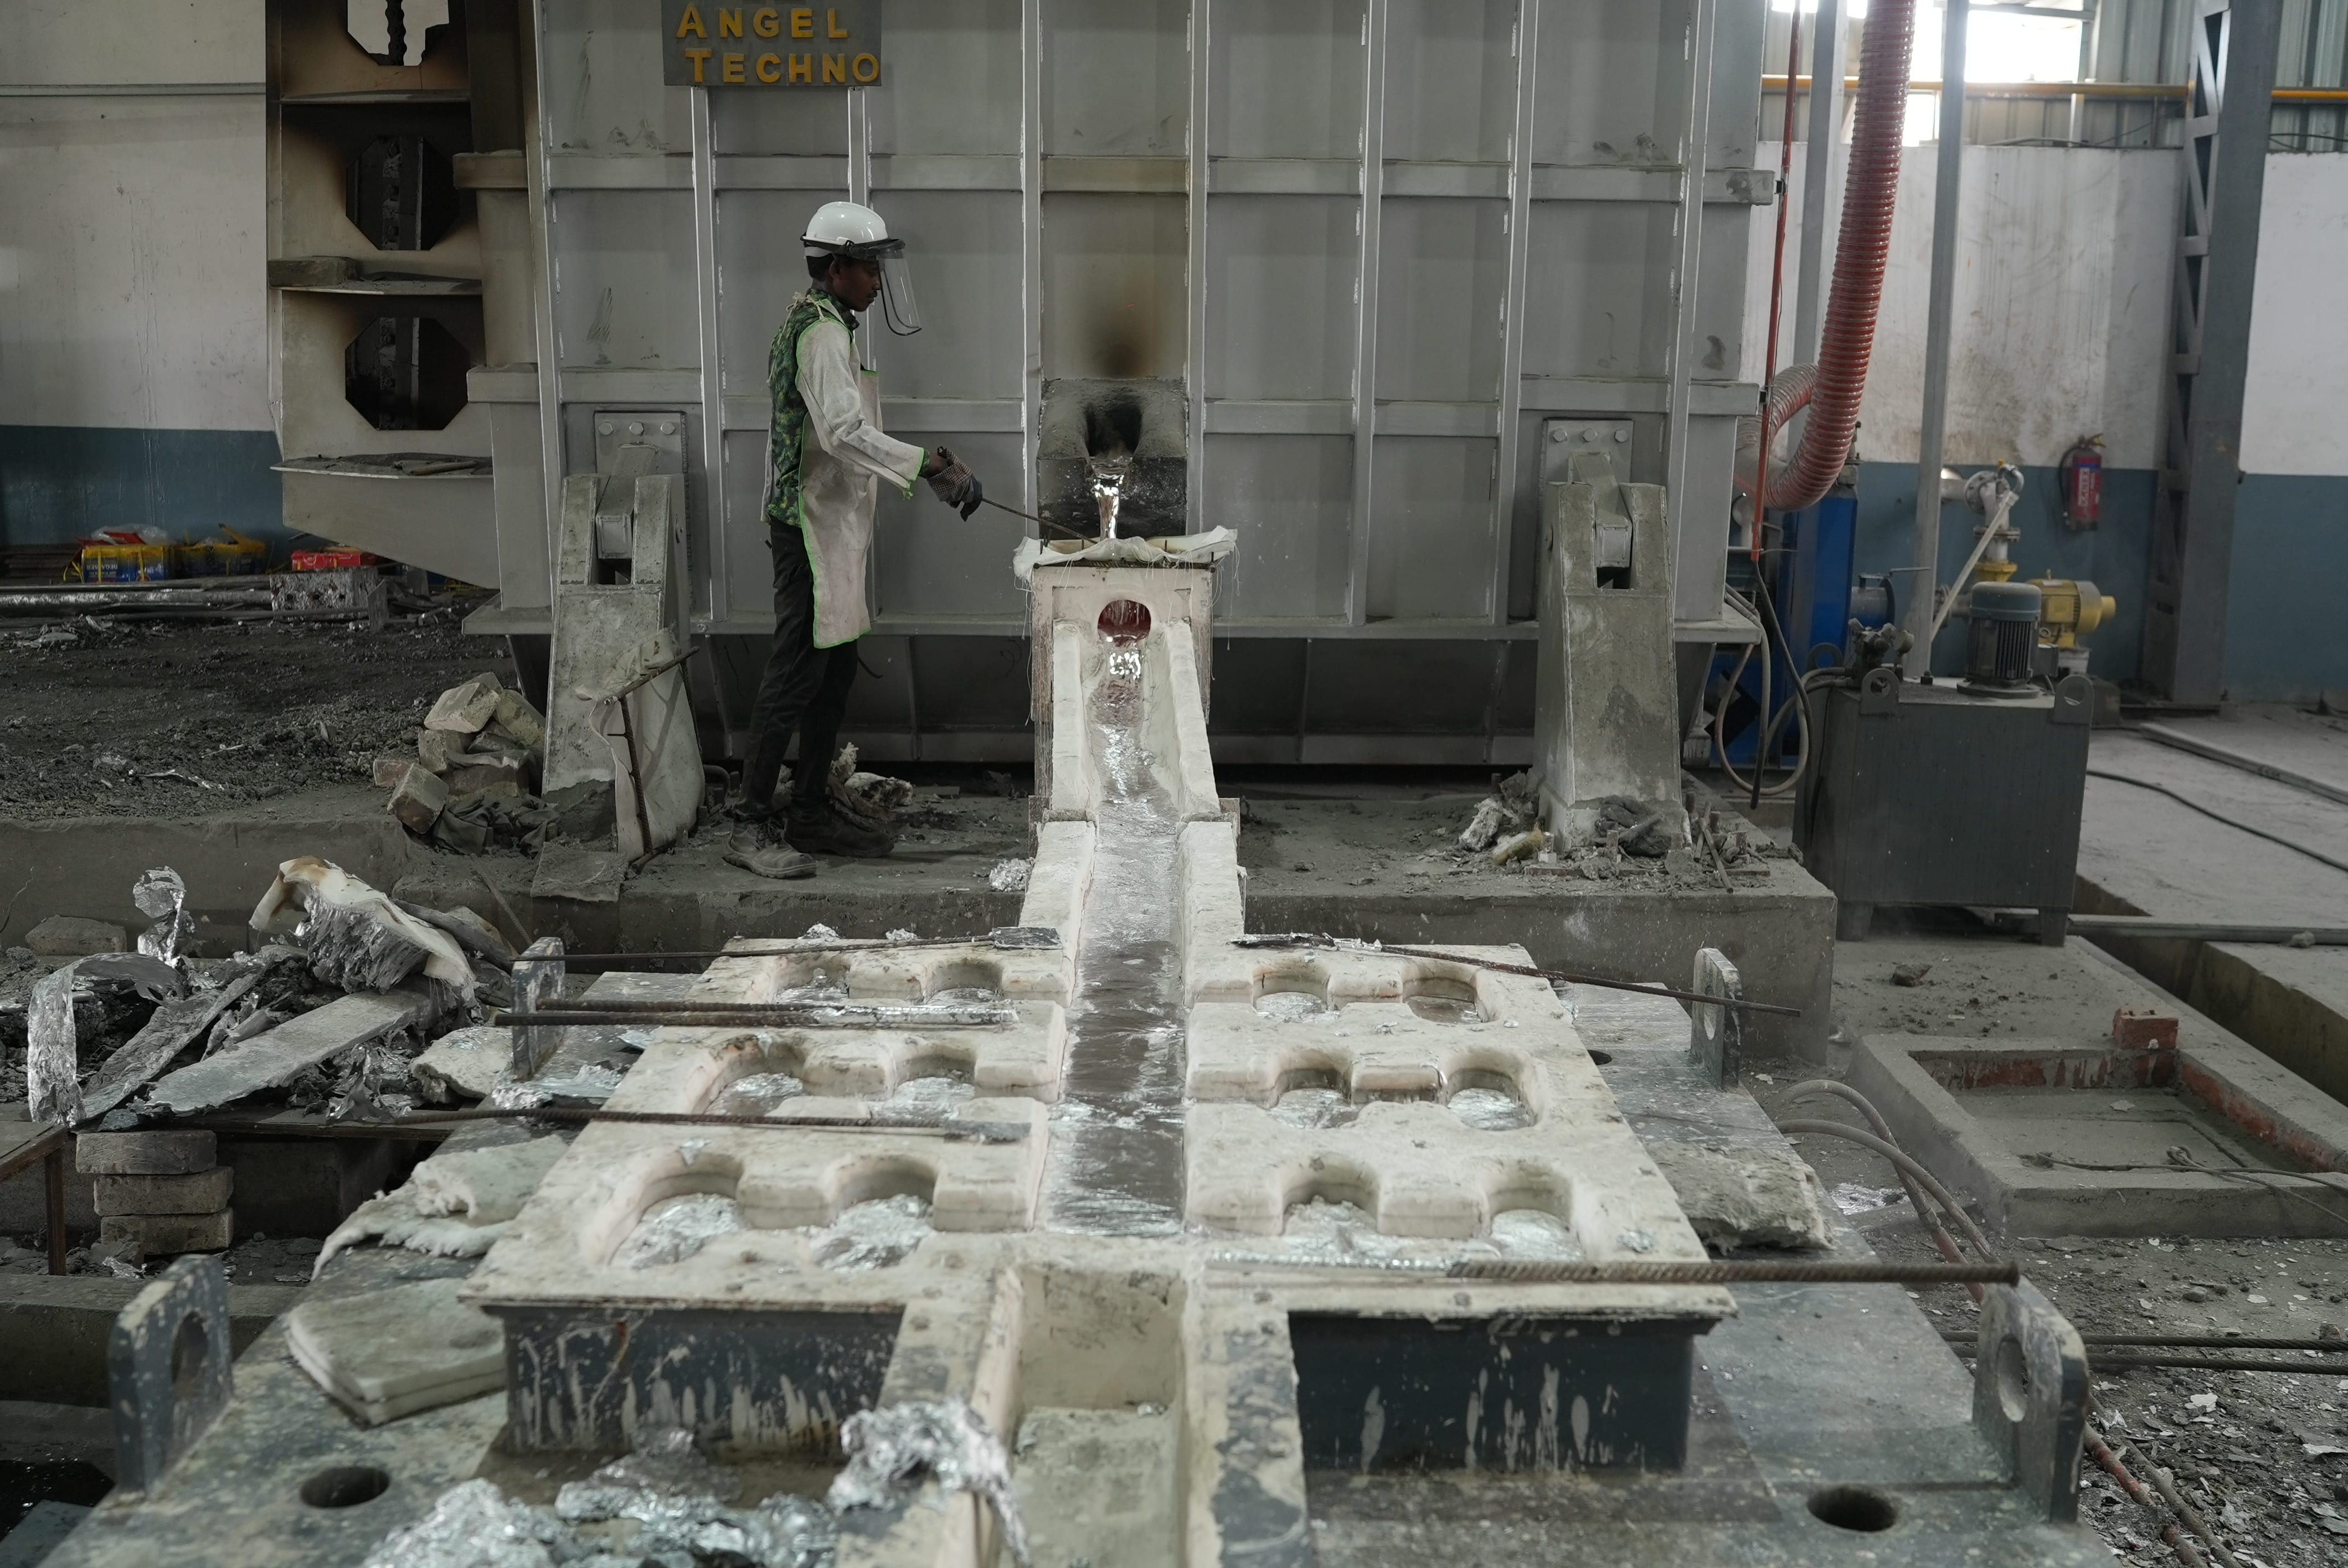
In-house prime alloy melting & hot-top billet casting line
Structural profiles engineered up to 300mm CCD envelope
In-house computerized wire-EDM die design & corrections
Heat-by-heat metallurgical chemistry & mechanical certs
Engineering Precision. Built for Industry.
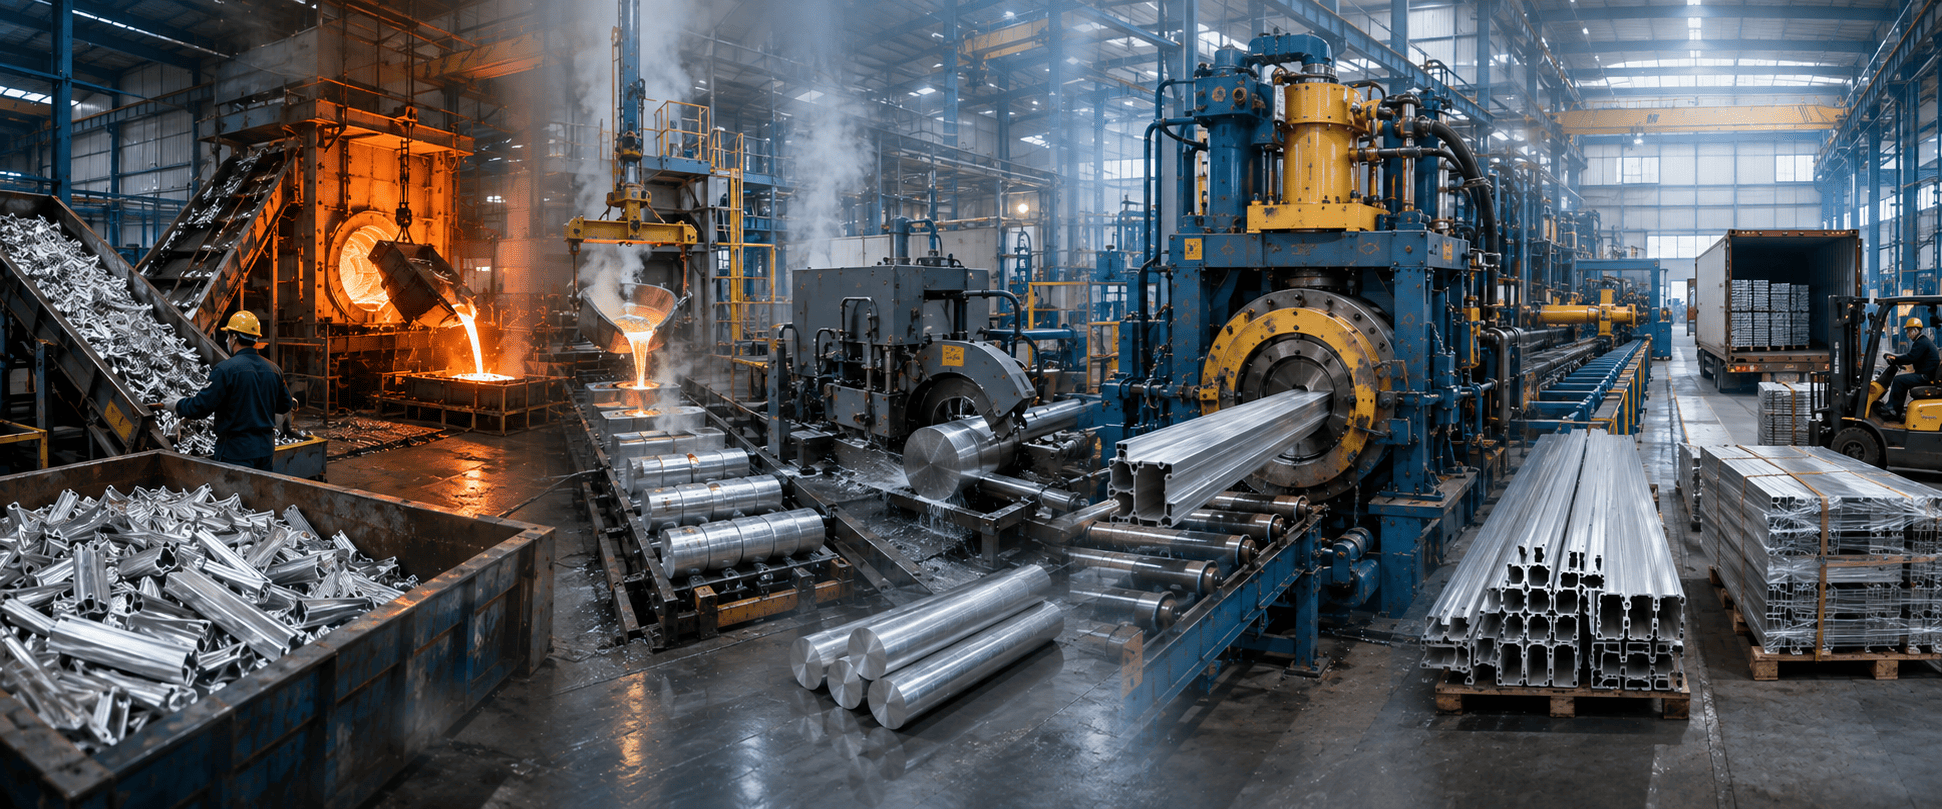
Astham Industries Pvt. Ltd. is a premier manufacturing enterprise in Gujarat, India, dedicated to the high-tonnage production of precision-engineered aluminium extrusion profiles.
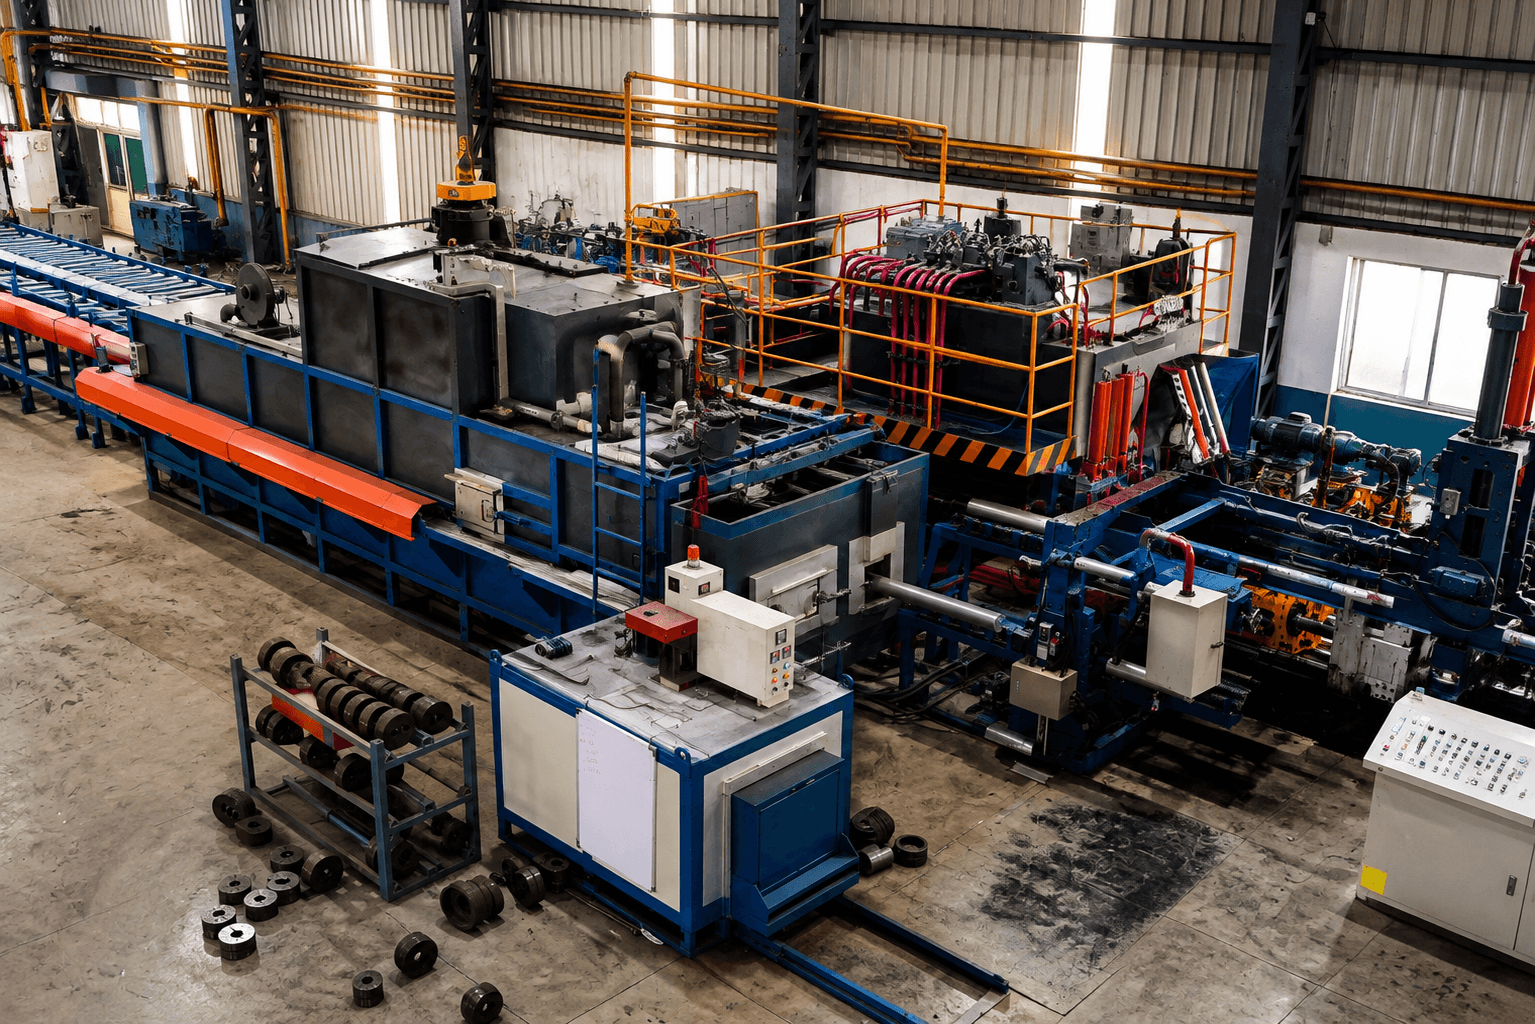
Operating state-of-the-art automated hydraulic presses, in-house wire-EDM die development shops, and computer-controlled artificial aging furnaces, we deliver tight-tolerance cross-sections for critical industrial applications.
Precision & Metallurgical Integrity
To manufacture zero-defect aluminium extrusion profiles through continuous metallurgical innovation, precision die tooling, stringent quality assurance, and customer-first engineering collaboration.
Sustainable Global Benchmark
To be recognized globally as the benchmark in high-precision aluminium manufacturing, empowering infrastructure, clean energy, and sustainable industrial growth.
Engineering Precision. Built for Industry.
Astham Industries Pvt. Ltd. is a premier manufacturing enterprise in Gujarat, India, dedicated to the high-tonnage production of precision-engineered aluminium extrusion profiles.
Operating state-of-the-art automated hydraulic presses, in-house wire-EDM die development shops, and computer-controlled artificial aging furnaces, we deliver tight-tolerance cross-sections for critical industrial applications.
Precision & Metallurgical Integrity
To manufacture zero-defect aluminium extrusion profiles through continuous metallurgical innovation, precision die tooling, stringent quality assurance, and customer-first engineering collaboration.
Sustainable Global Benchmark
To be recognized globally as the benchmark in high-precision aluminium manufacturing, empowering infrastructure, clean energy, and sustainable industrial growth.
HIGH-TONNAGE EXTRUSION CAPACITY
IN-HOUSE DIE DESIGN & DEVELOPMENT
TIGHT TOLERANCE PRECISION
ISO 9001:2015 & CE CERTIFIED
TRUSTED BY CLIENTS WORLDWIDE
Industries We Serve
Featured Engineered Profiles
Standard and custom aluminium cross-sections engineered for structural rigidity, thermal performance, and tight tolerances.
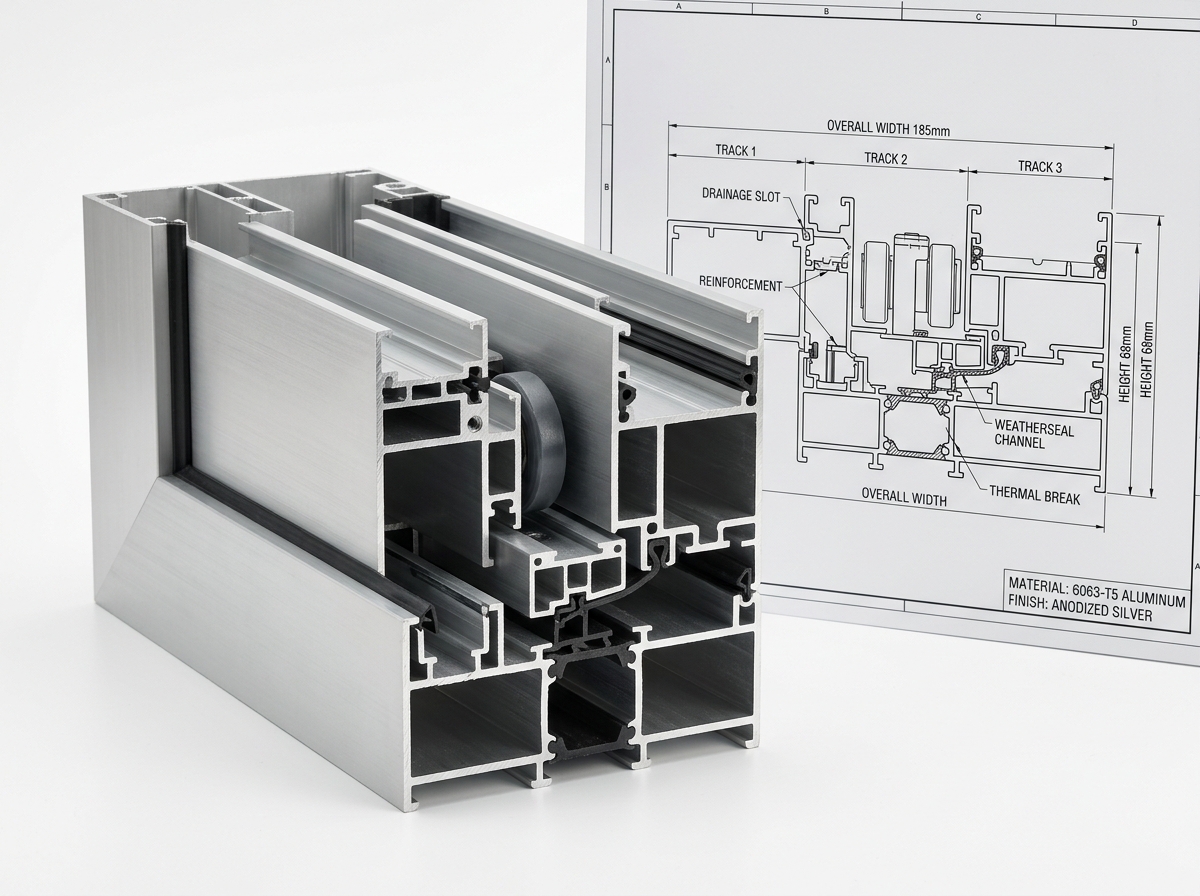
Heavy Sliding Door & Window System Profile
Multi-track sliding door aluminium sections with reinforced interlocks and precision roller tracks for silent, effortless operation.
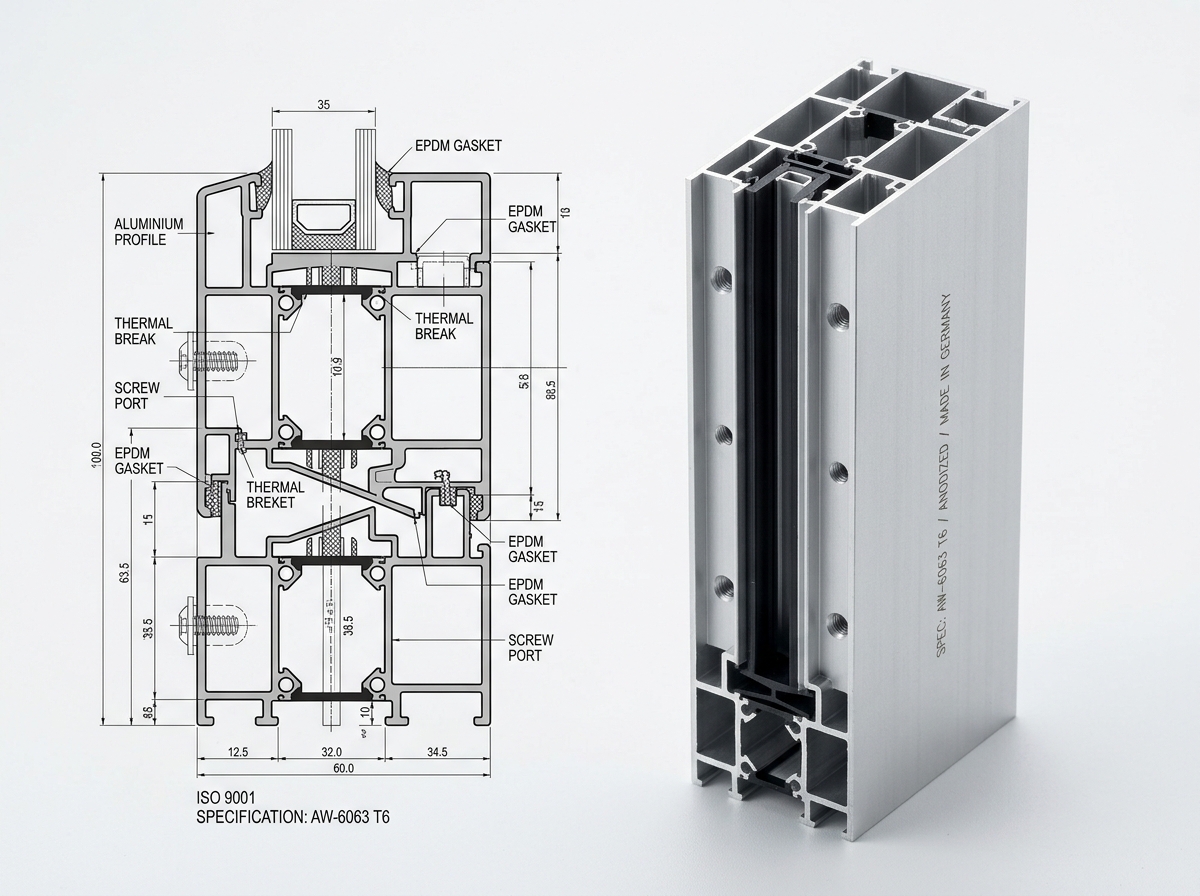
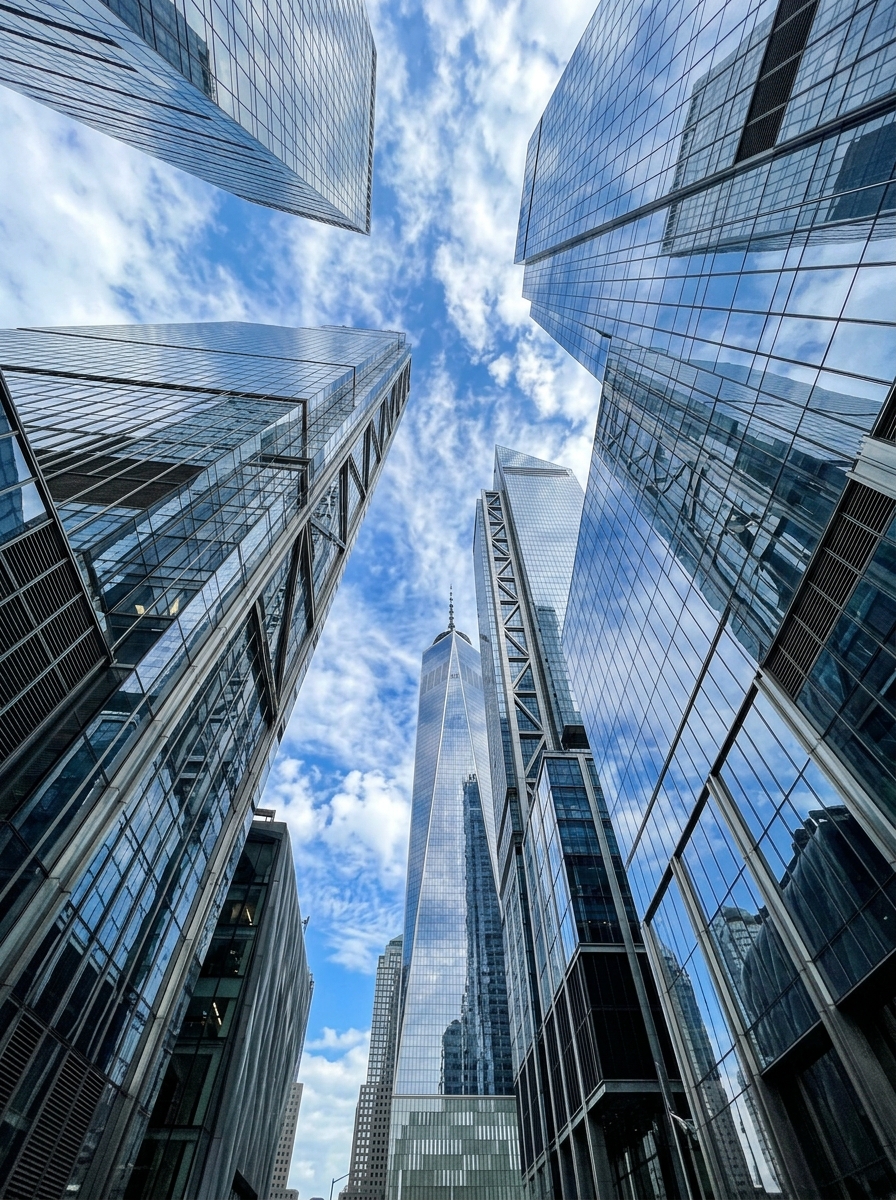
Structural Curtain Wall Mullion & Transom Profile
Heavy-duty structural aluminium profiles engineered for unitized and semi-unitized architectural glass curtain wall façade systems.
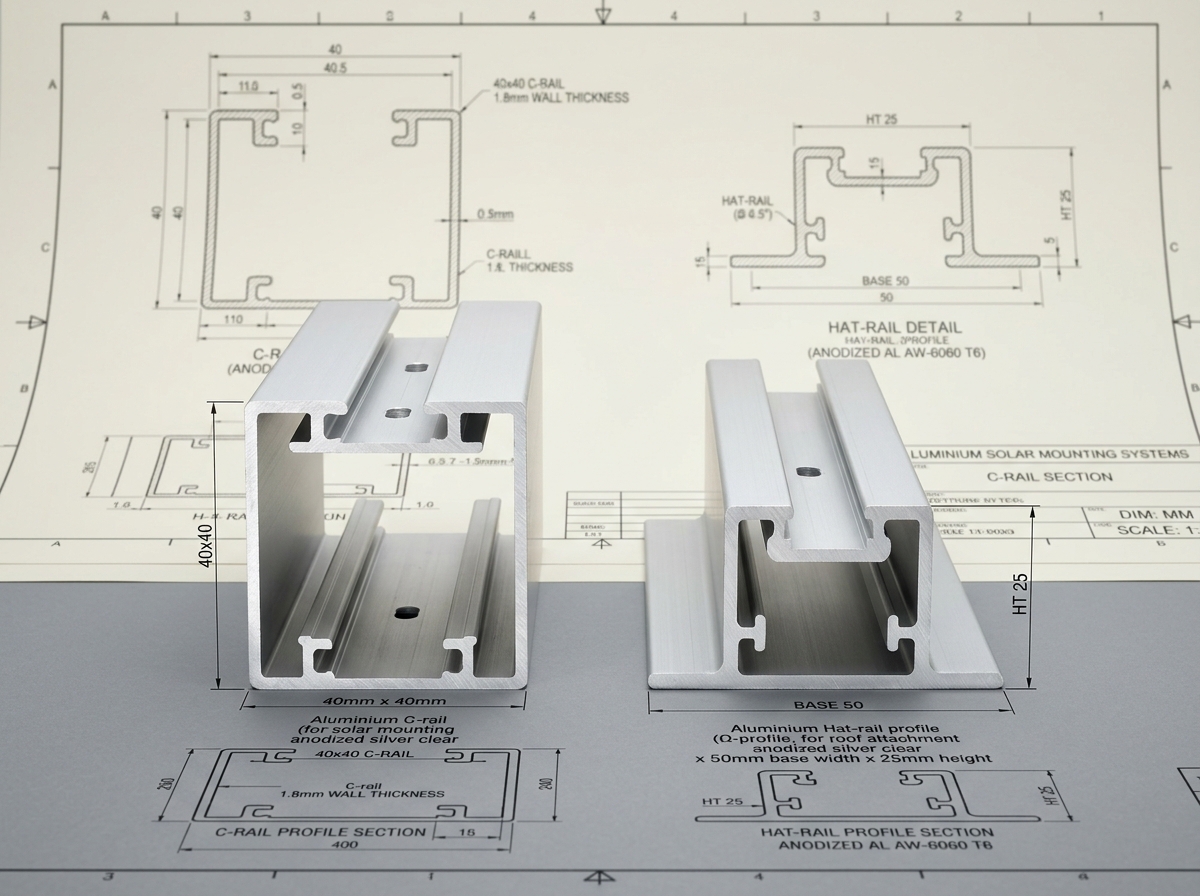
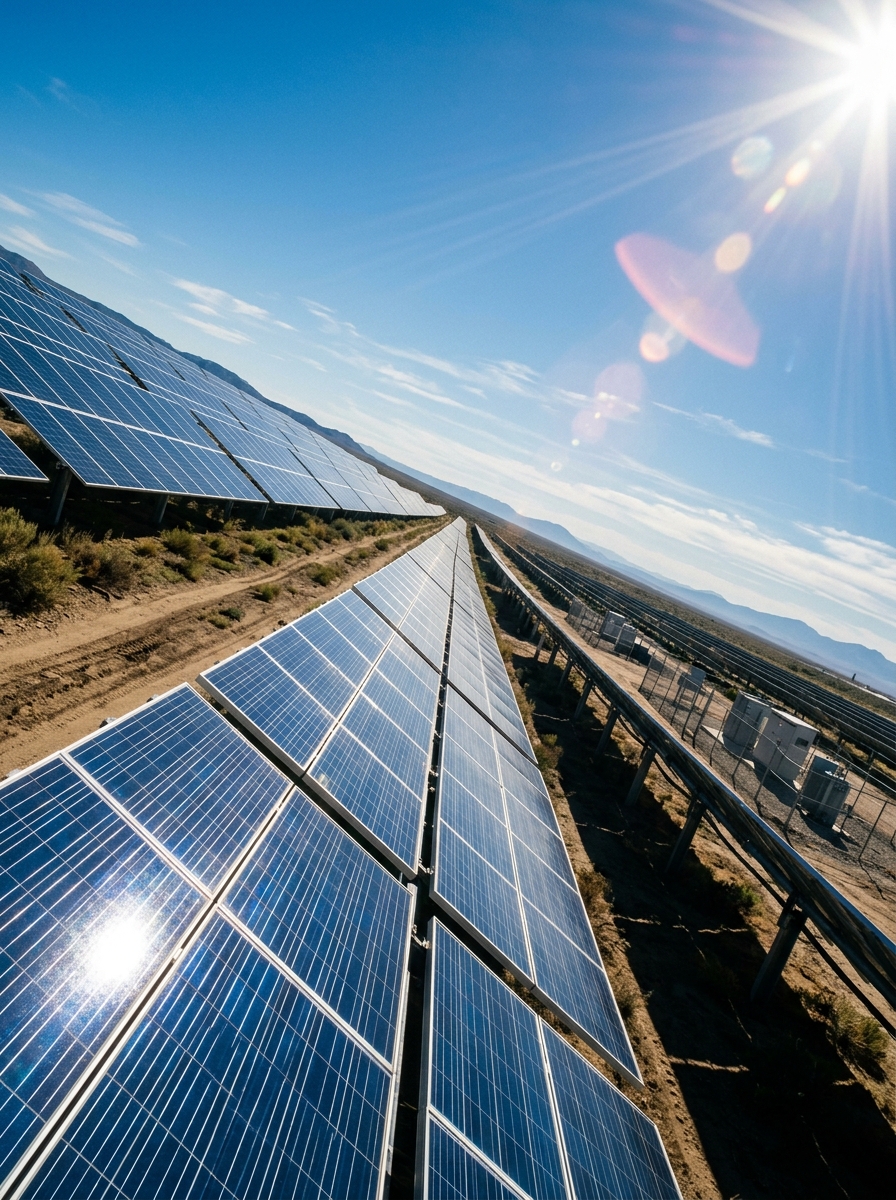
Heavy Solar Module Mounting Rail Profile (C-Rail & Hat Rail)
High-strength structural aluminium mounting rails engineered for high-wind rooftop and ground utility solar installations.
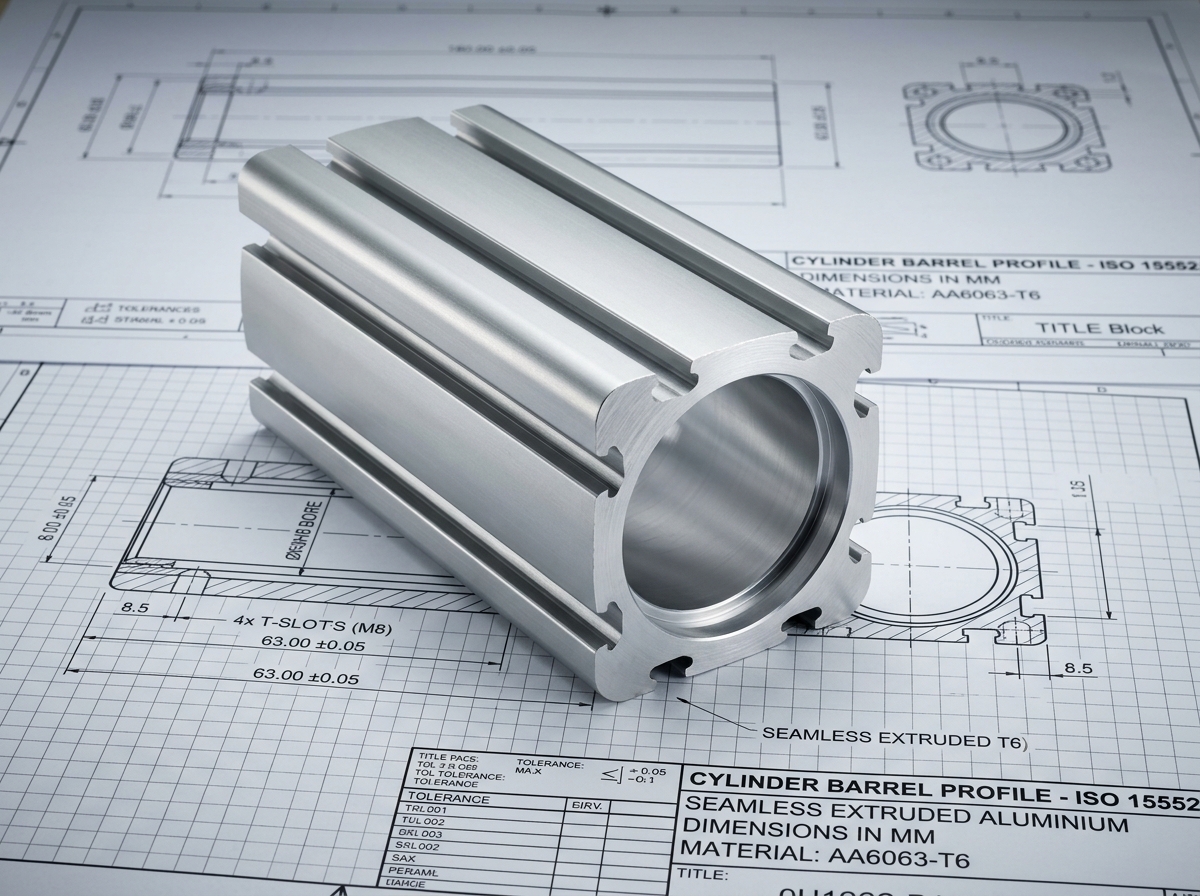
Precision Pneumatic Cylinder Barrel Profile
Seamless internal bore aluminium extrusion tubes with mirror hard-anodized inner surfaces for pneumatic and hydraulic actuators.
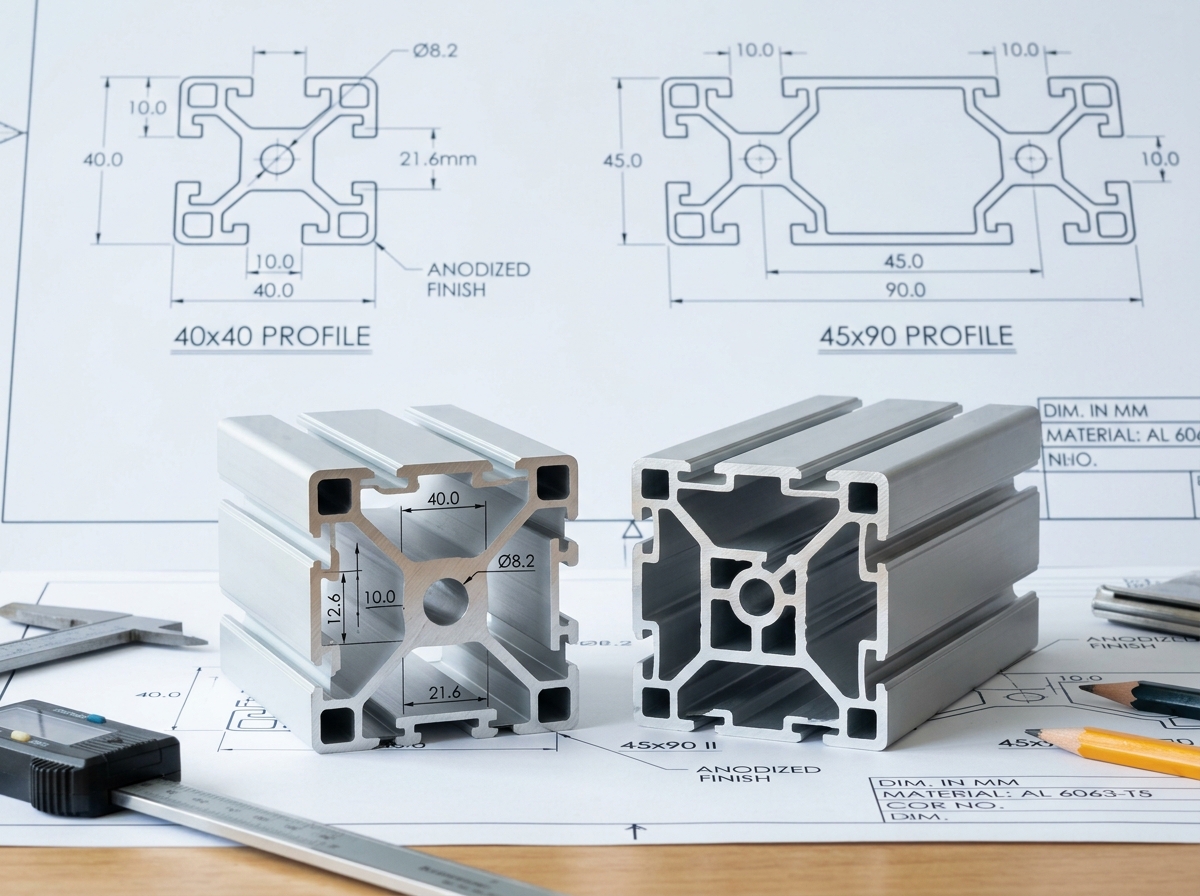
Heavy Duty T-Slot Modular Framing Profile (40x40 & 45x90)
Versatile structural modular aluminium framing sections for machinery enclosures, workbenches, and assembly conveyors.
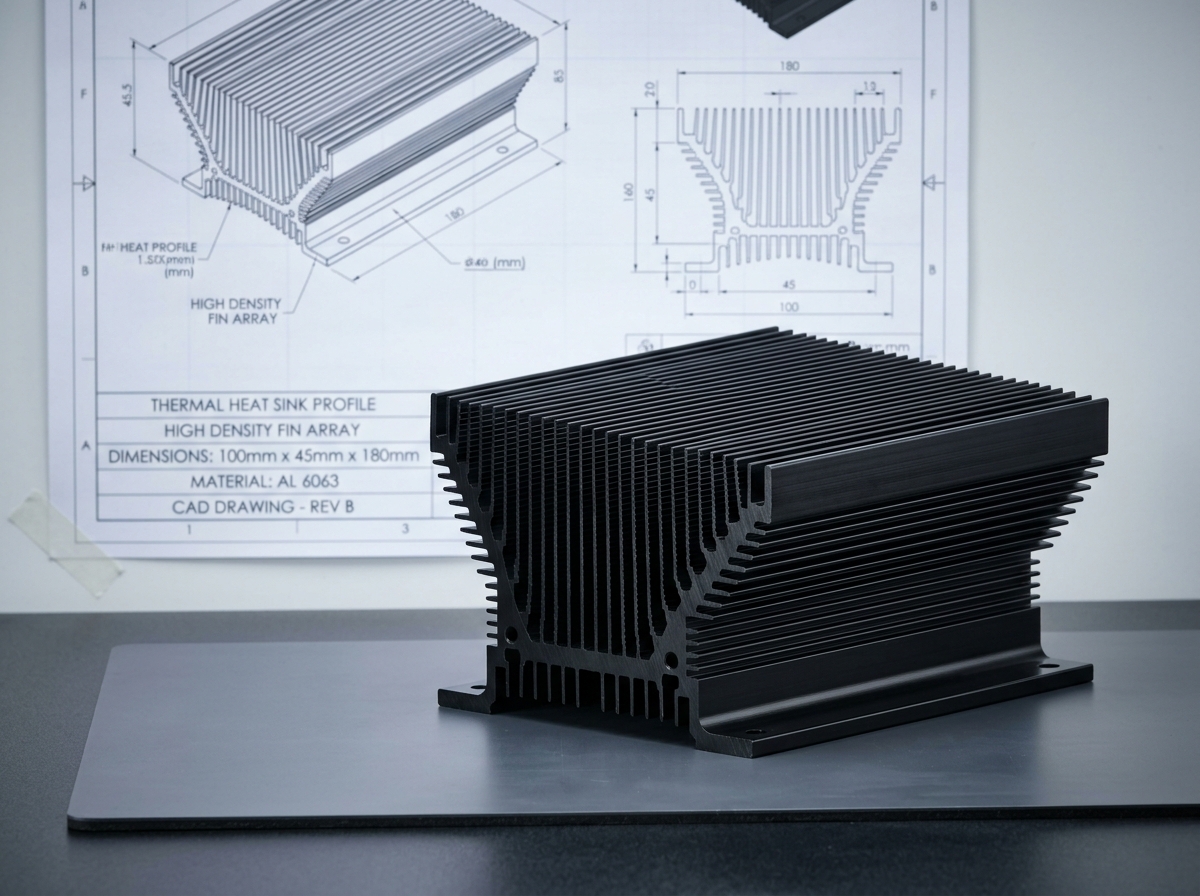
High-Density Comb Profile Heat Sink
High aspect ratio dense finned aluminium heat sinks for high-power semiconductors and inverter electronics.
Key Stages of Our Precision Extrusion Workflow
From prime virgin billet preheating and nitrogen-cooled extrusion to computerized precision quenching, tension stretching, and OES spectrometer verification.
Raw Material Inspection & Billet Preheating
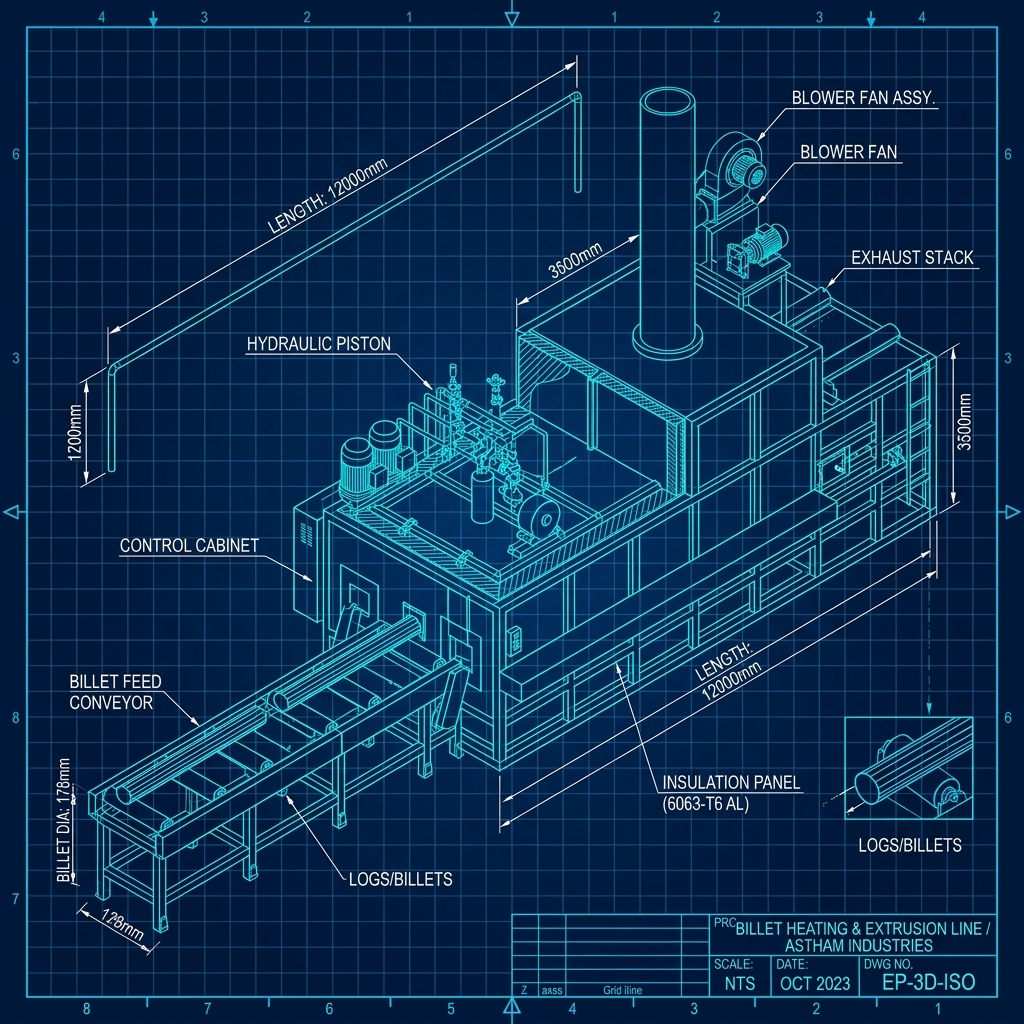
Only primary virgin aluminium billets (A8 grade, 99.7% purity) from certified primary smelters are used. Billets are ultrasonically tested for inclusions and heated in automated gas-fired gradient log heaters to 450°C - 480°C.
Precision Die Design & Tool Heating
Custom extrusion dies manufactured in-house on high-precision CNC Wire-EDMs are inspected and soaked in die ovens at 460°C to match billet temperature, preventing thermal shock and surface defects.
Hydraulic Extrusion Pressing
The heated billet is sheared and forced under immense hydraulic pressure (up to 1,800 Metric Tons) through the steel die aperture, flowing plasticized metal into complex hollow or solid geometries.
Intensive In-Line Quenching
As the profile exits the die at speeds up to 50 meters per minute, it is rapidly cooled using controlled high-velocity water mist and forced air jets to lock in alloy alloying elements into solid solution.
Cooling Table & Automatic Pulling
Profiles are guided onto wide graphite slat handling tables by computerized pullers, ensuring zero scratch marks, minimal twist, and uniform cooling down to handling temperature.
Hydraulic Tension Stretching & De-Twisting
Profiles are clamped at both ends in hydraulic stretching machines and pulled under tension (0.5% - 1% controlled elongation) to achieve absolute straightness and relieve internal extrusion stresses.
Precision CNC Saw Cutting
Stretched profiles are conveyed to automated high-speed carbide saws and cut to exact mill lengths or customized client lengths with tight length tolerances (±1.0 mm).
Artificial Ageing Heat Treatment
Cut profiles are loaded into thermostatically regulated precipitation hardening ageing ovens and soaked at 180°C - 200°C for 6 to 8 hours to attain peak T5 or T6 temper mechanical strength.
Quality Lab Clearance, Wrapping & Dispatch
Every batch is tested for Webster hardness, tensile strength, and coating thickness. Profiles are interleaved with protective paper, shrink-wrapped, and packed in wooden crates for safe transport.
Surface Finishing (Anodizing / Powder Coating)
Profiles undergo automated 10-stage chemical pre-treatment followed by either multi-tank computerized Anodizing (10-25 micron) or electro-static thermosetting Powder Coating.
Plant & Facility Gallery
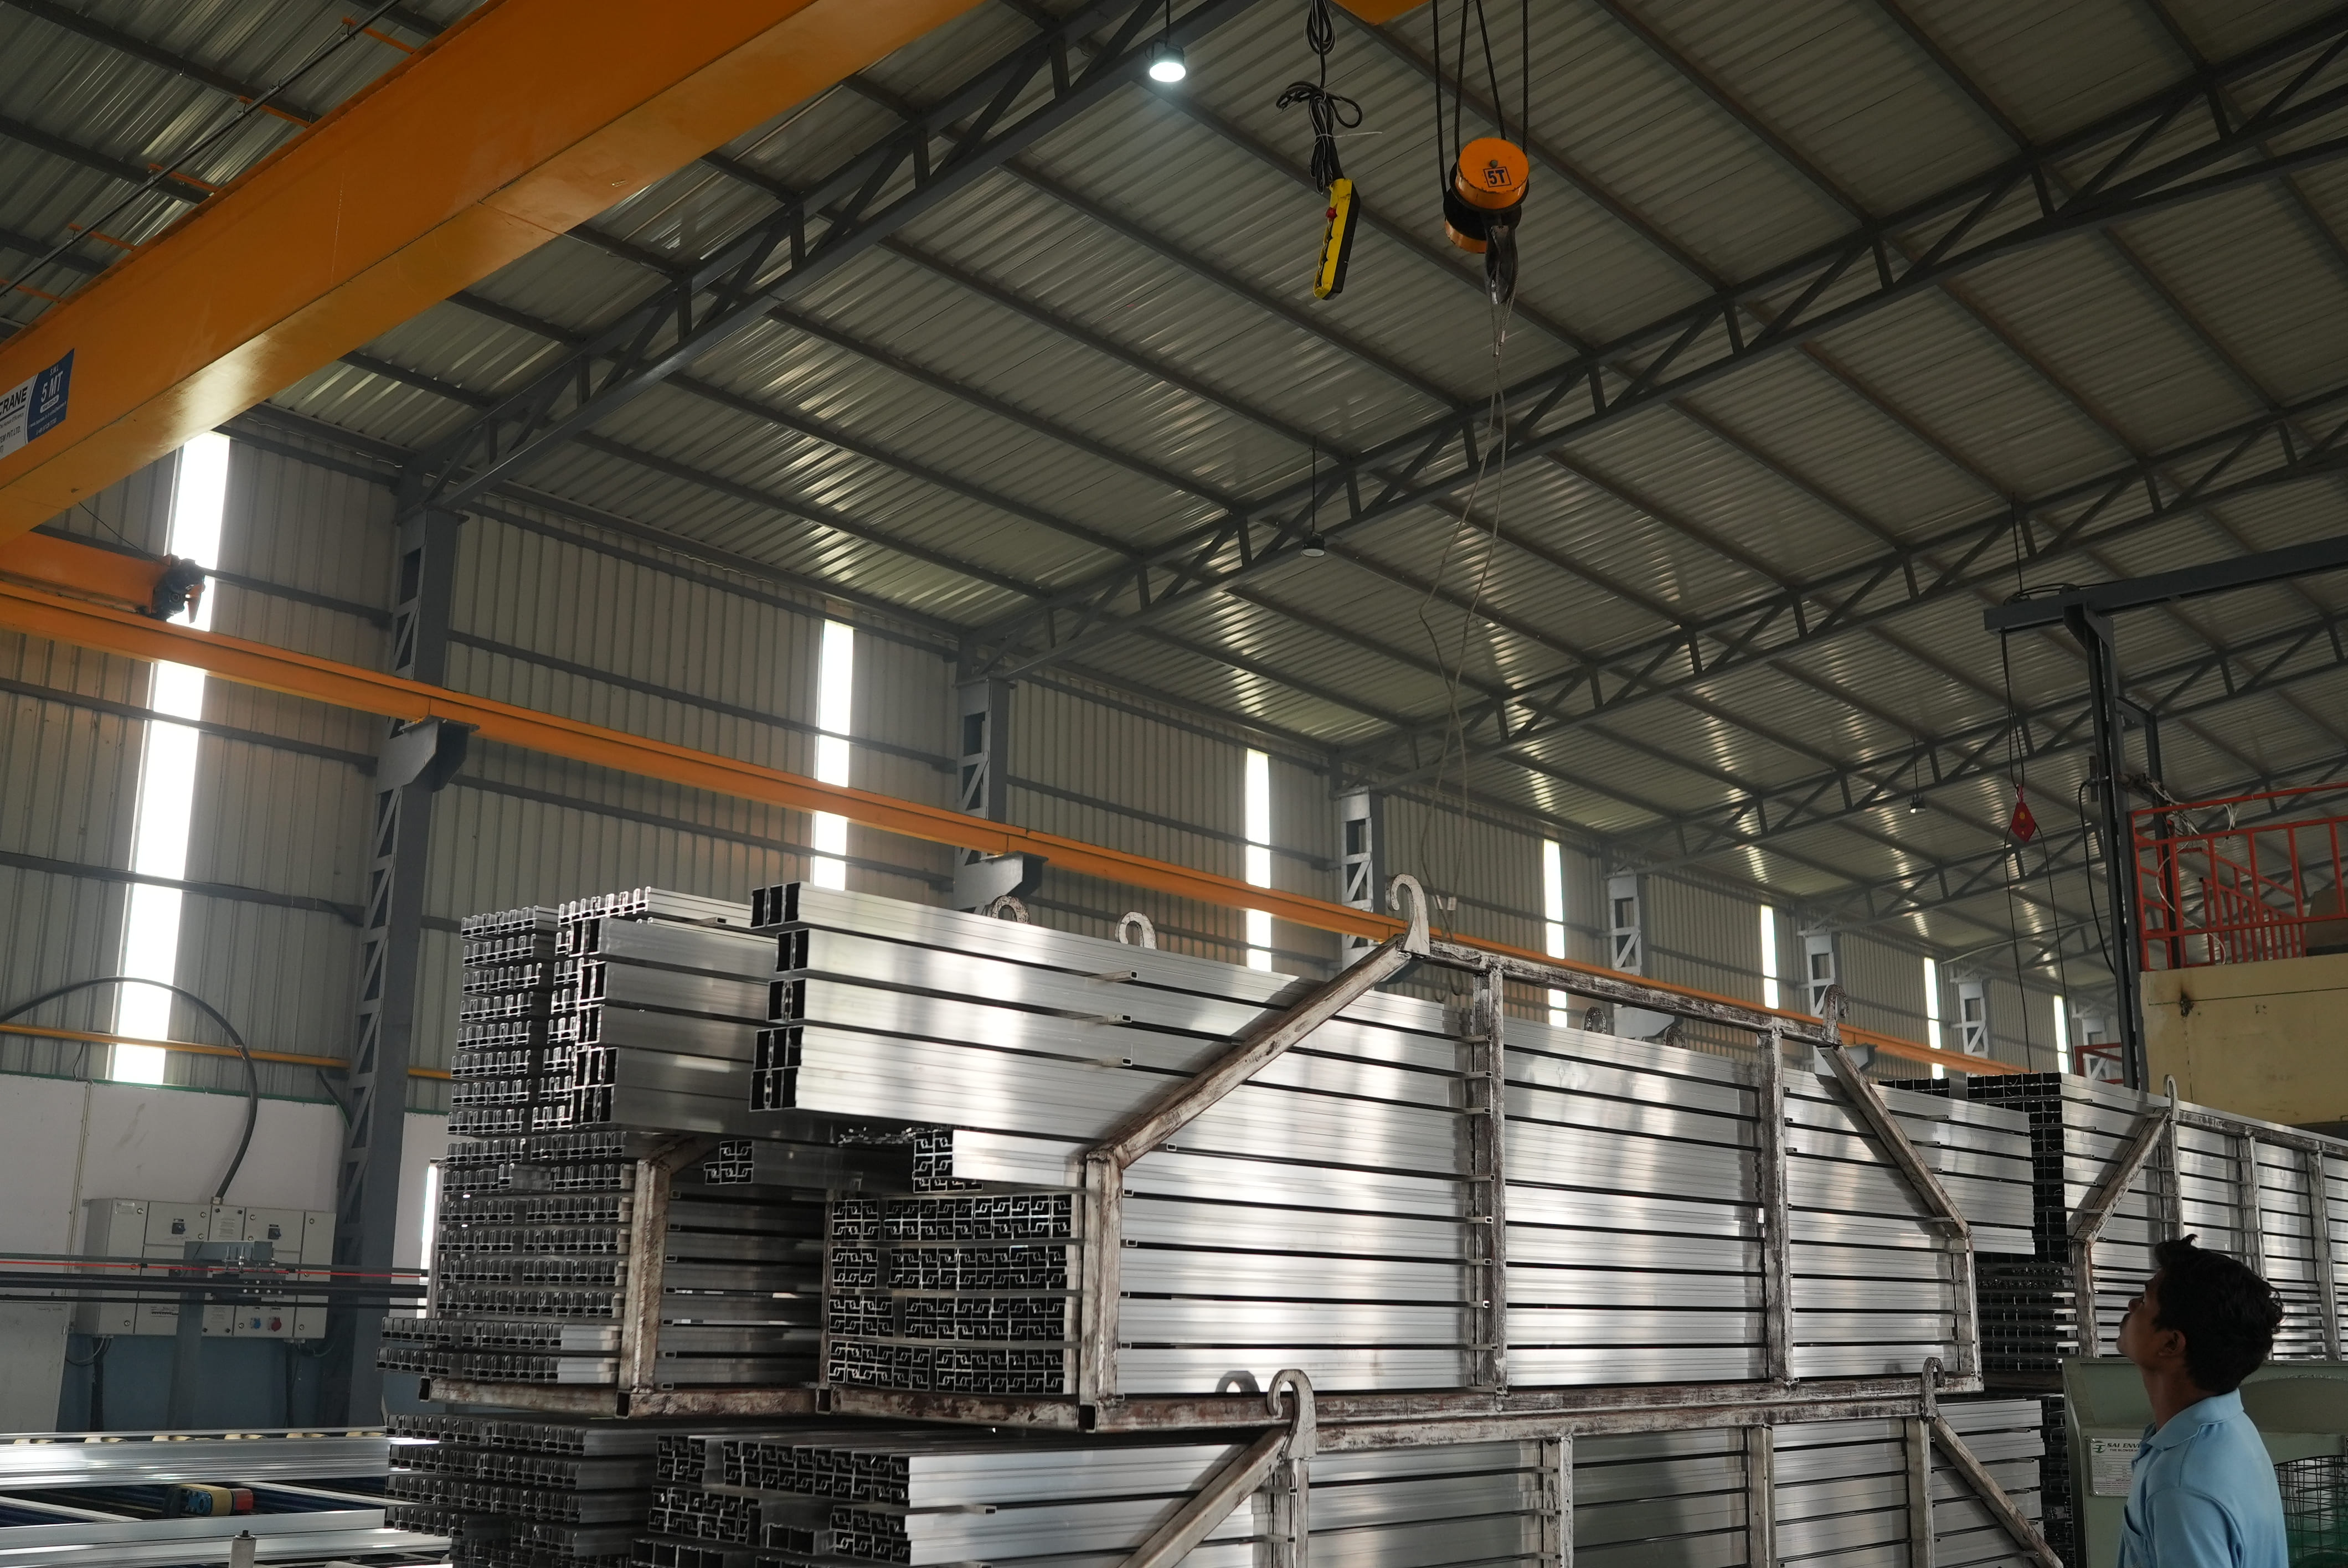
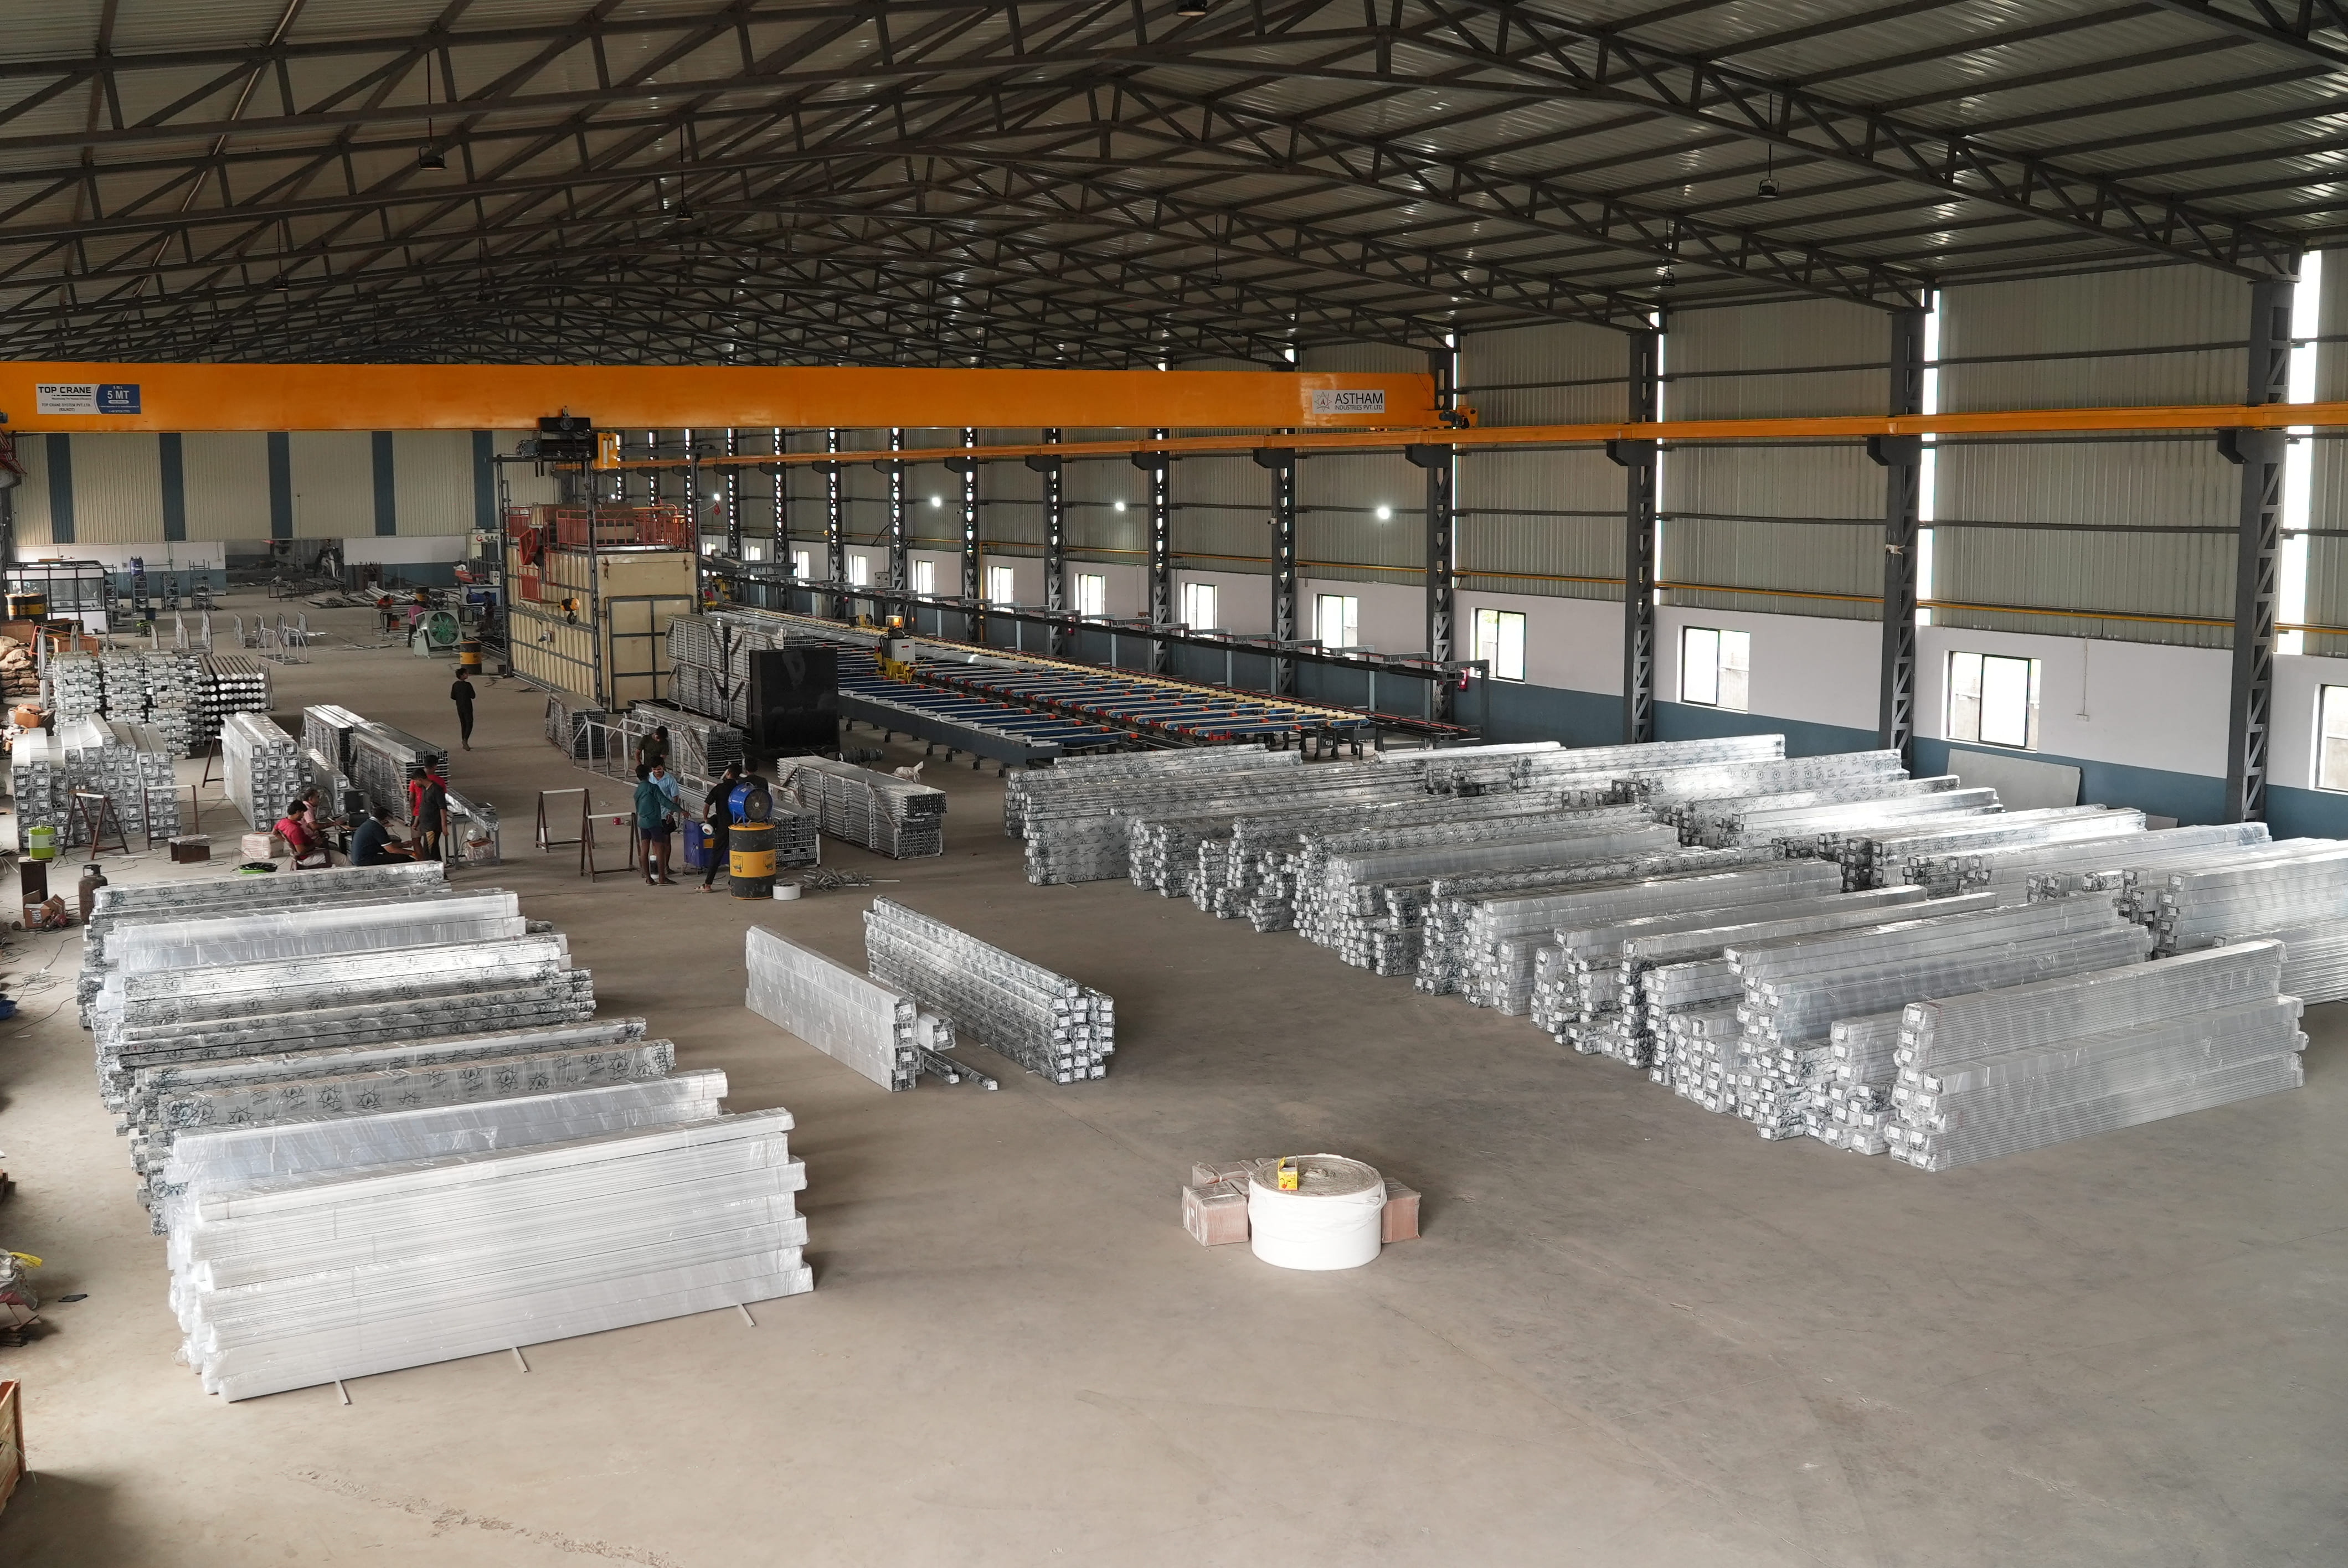
Inspect our extrusion bays, aging ovens, wire-EDM die shop, and metallurgical quality testing lab in operation.
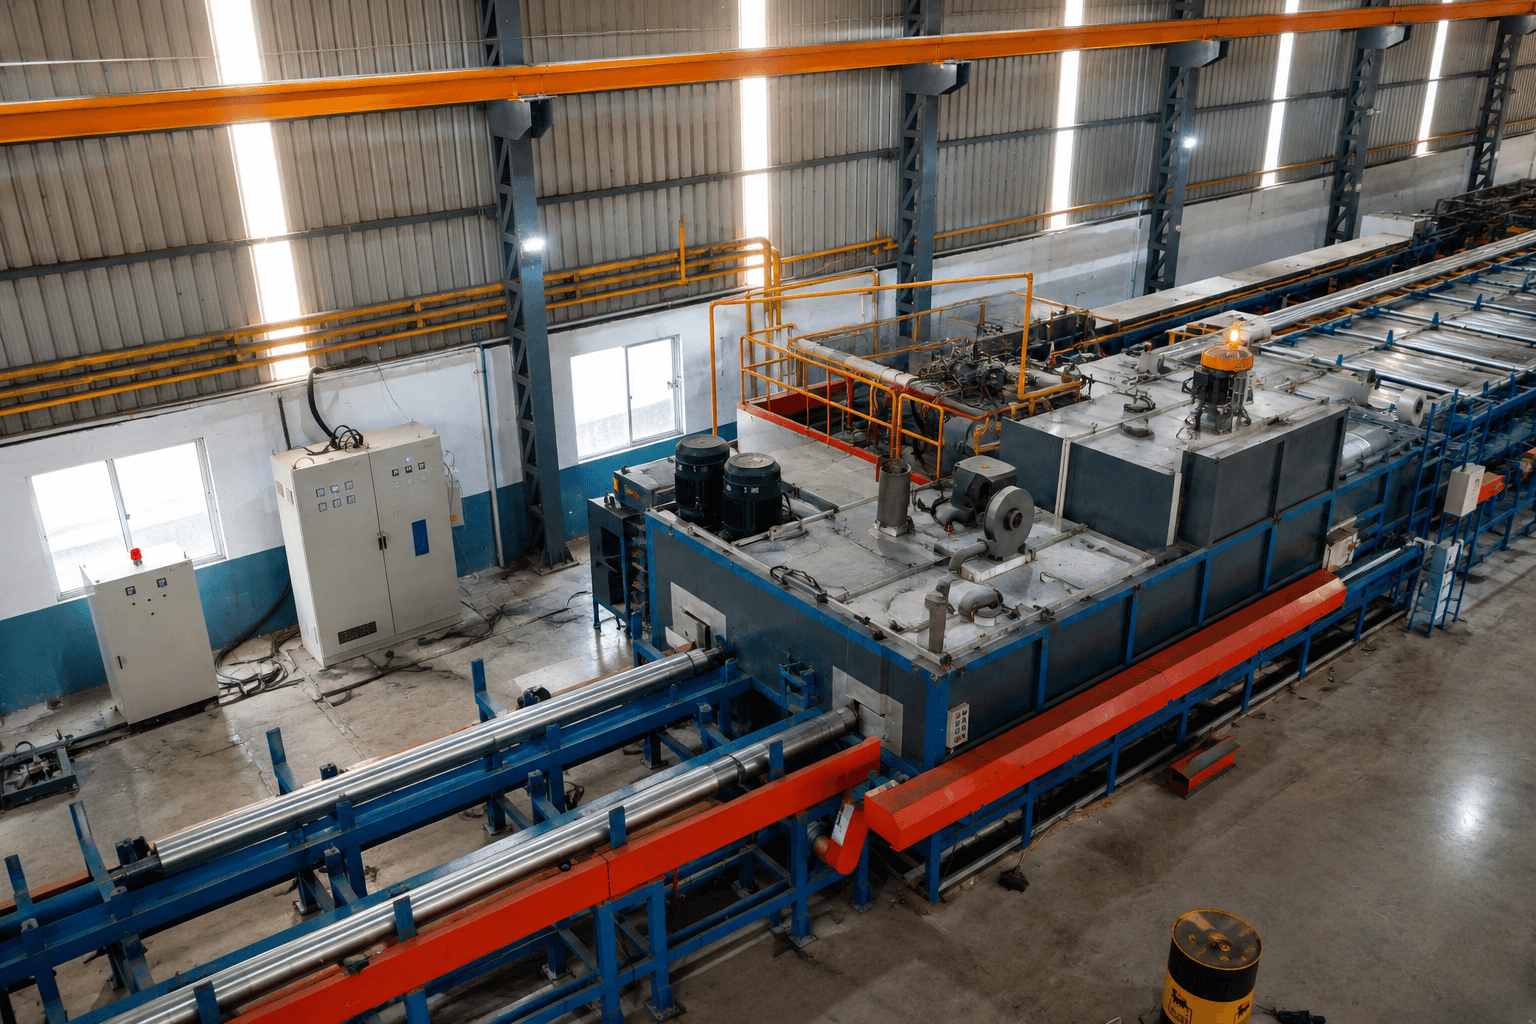
Billet Casting
Billet Hitter
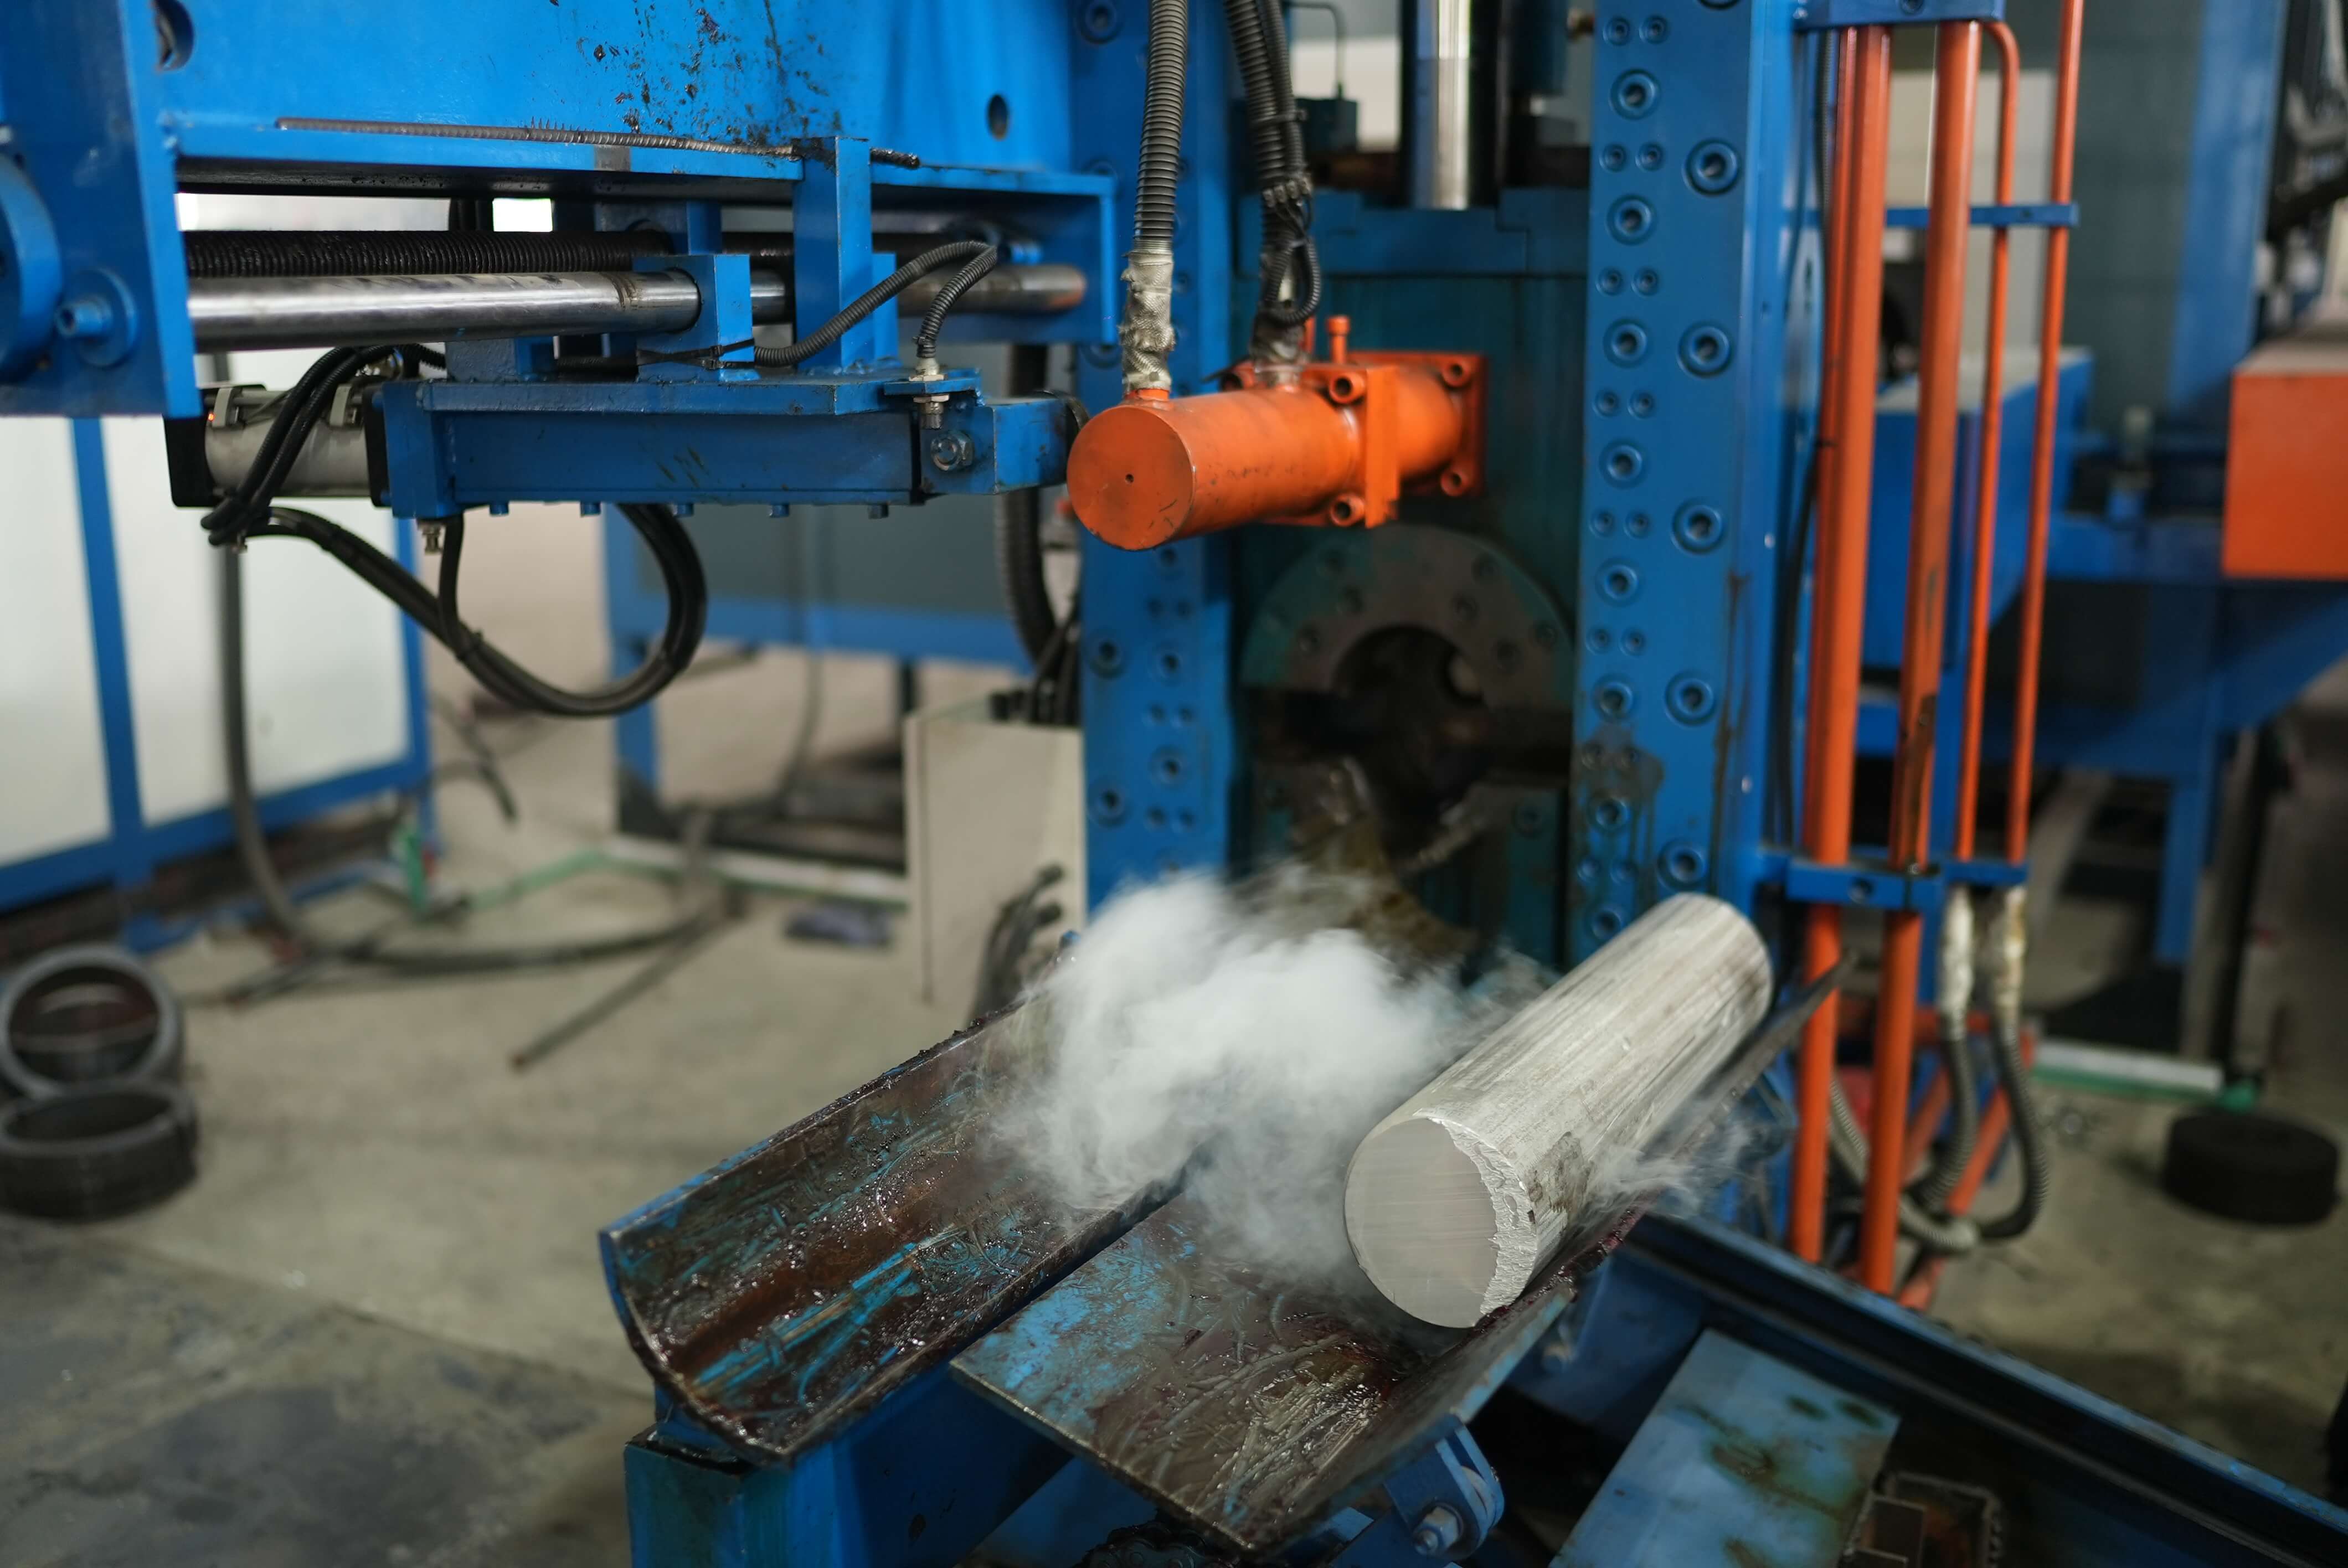
Billet Shear
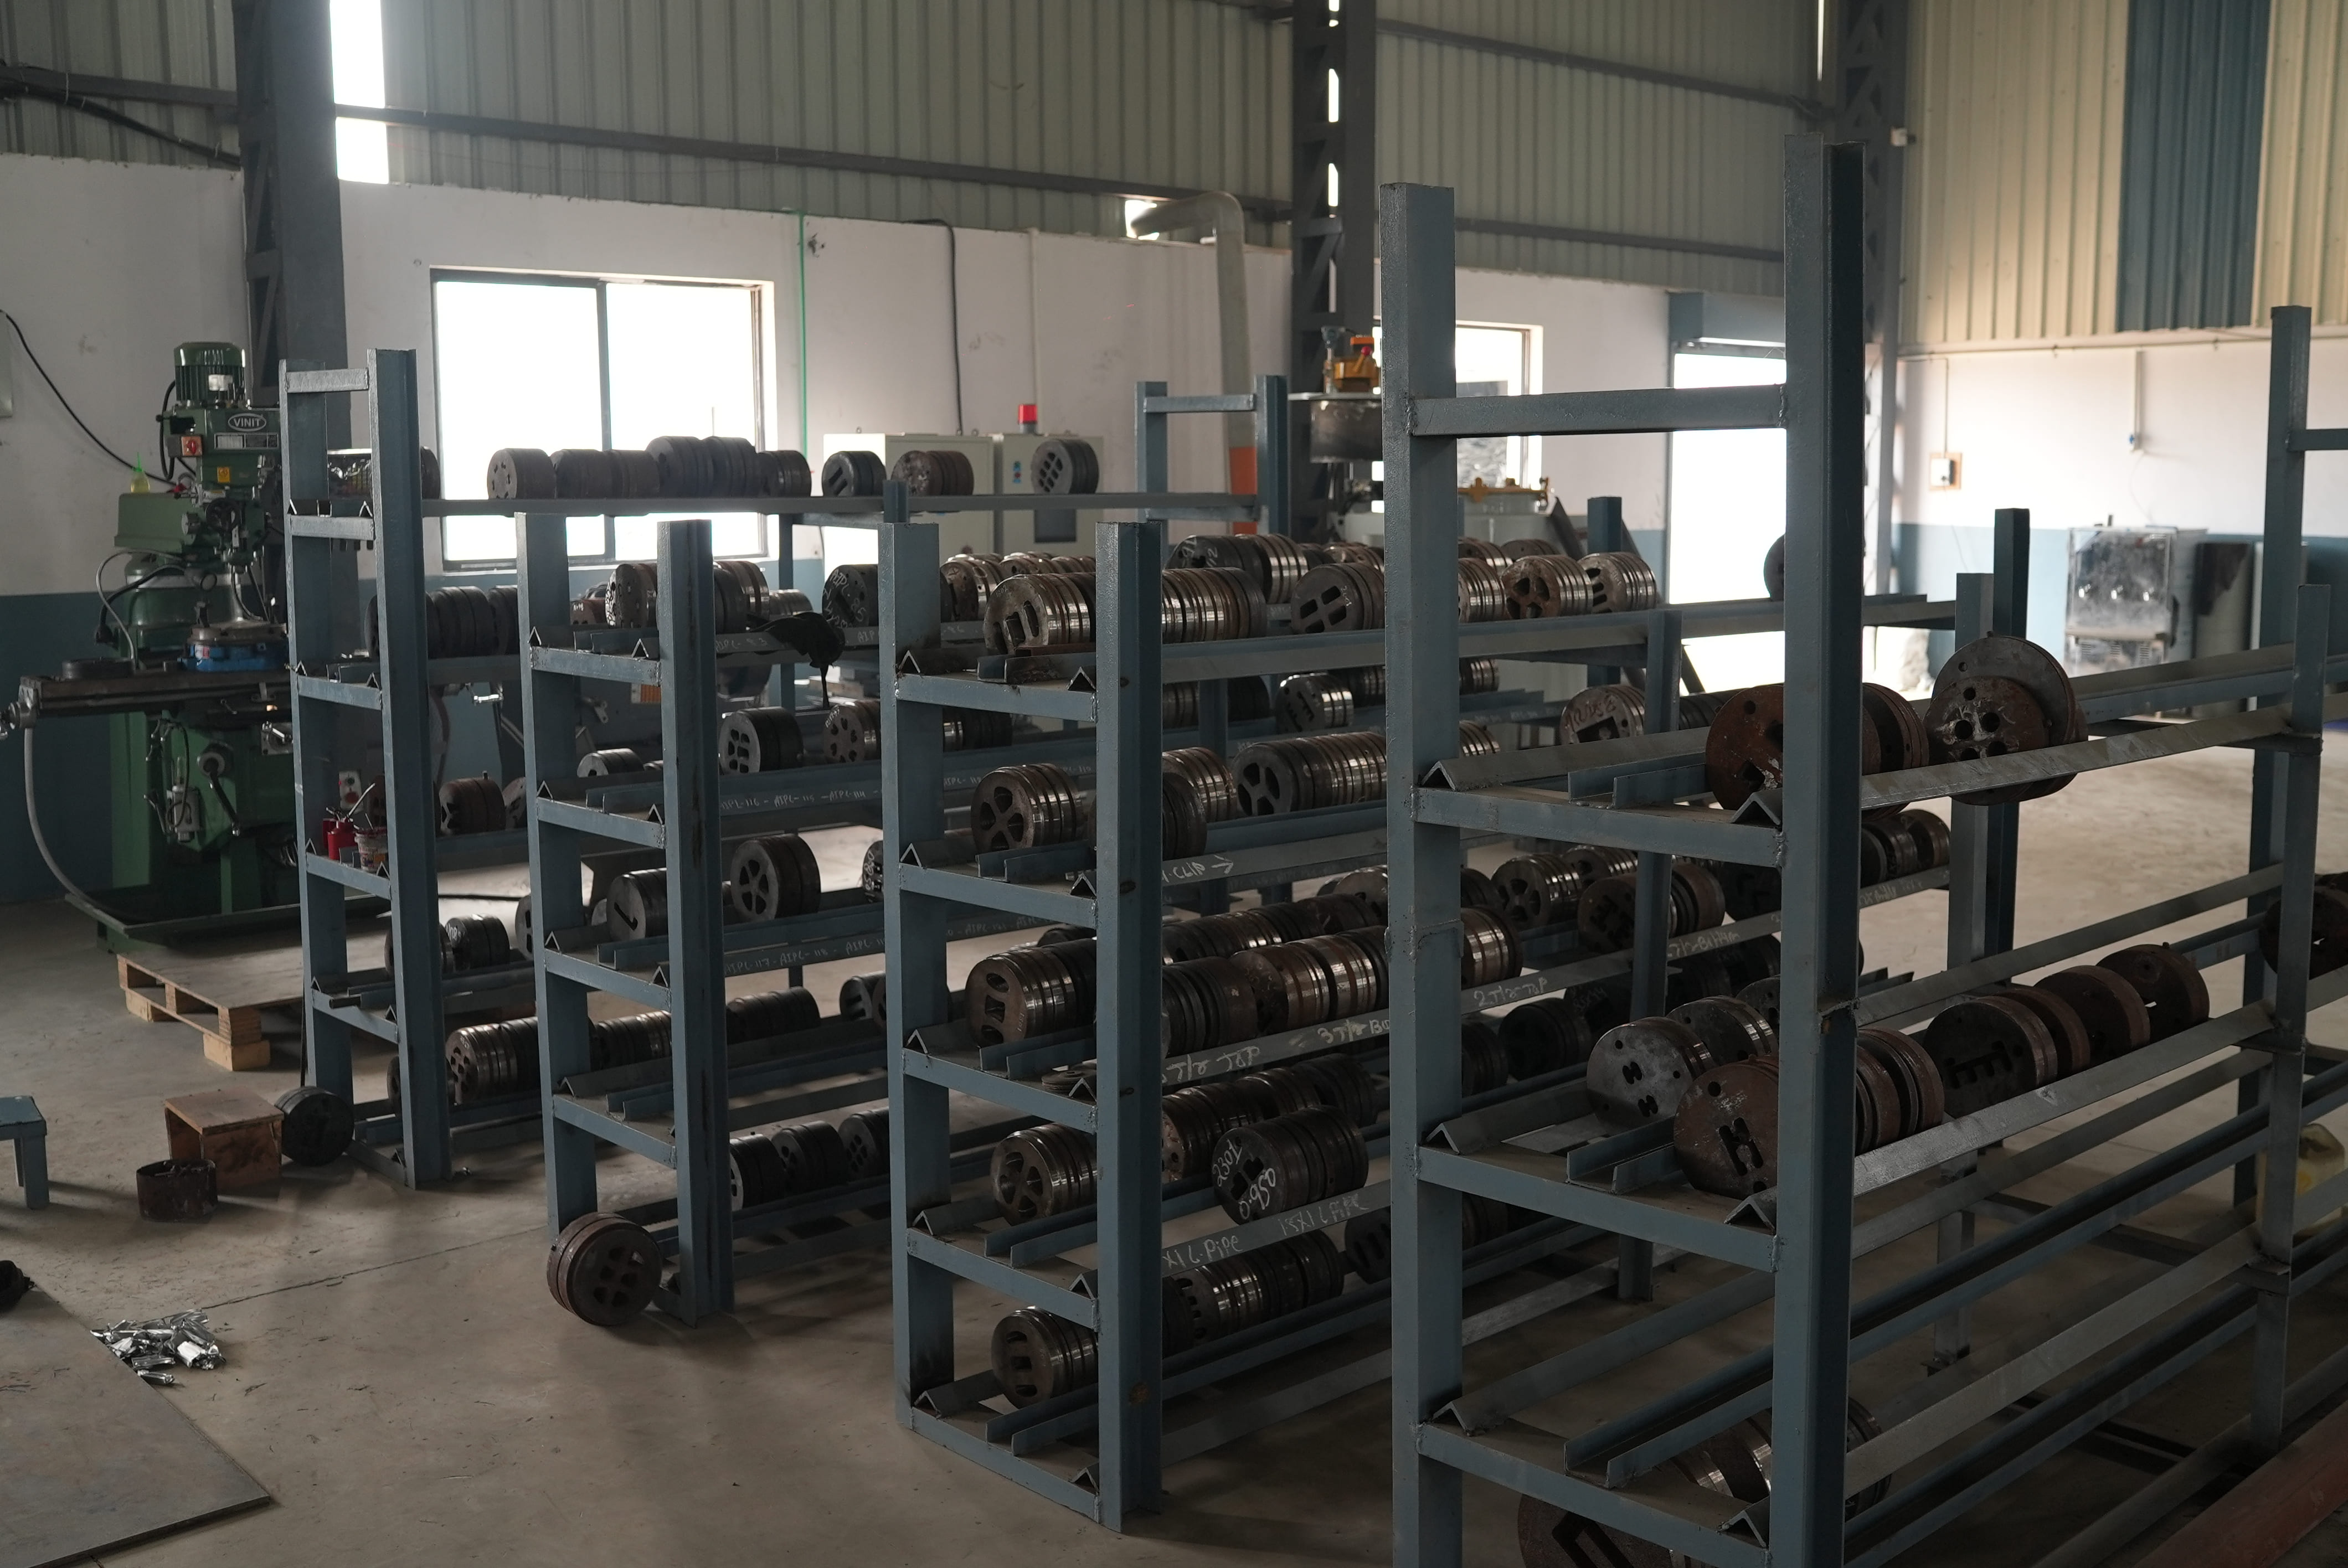
Dies & Tools Room
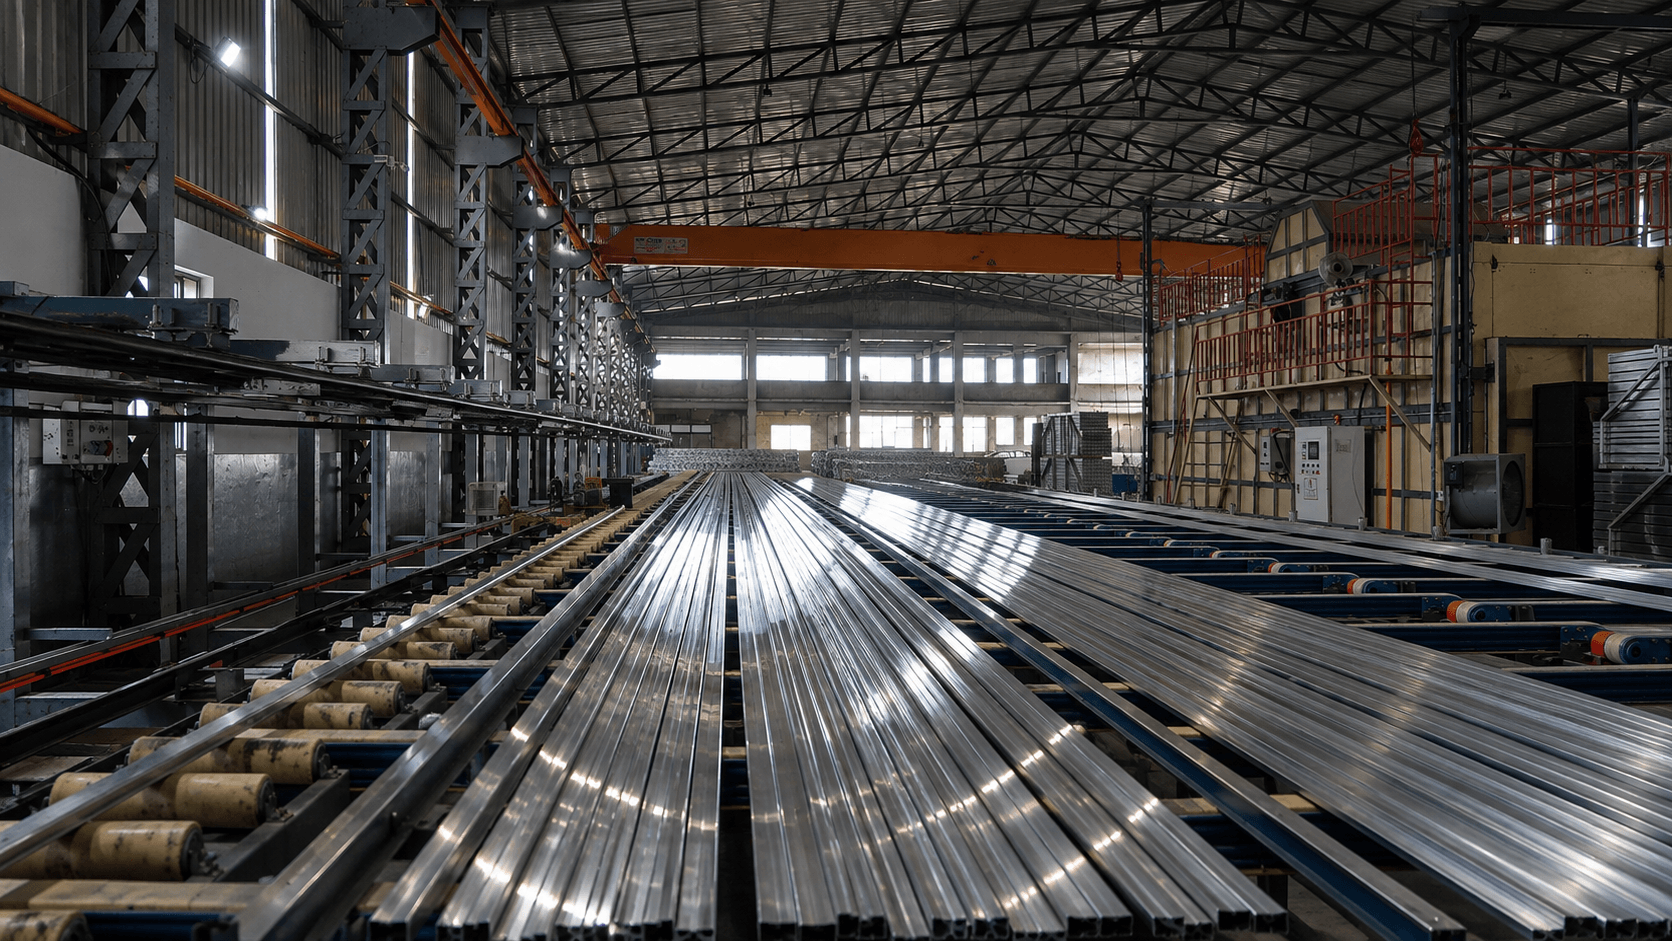
Handing Table
Hydraulic Extrusion Press
Billet Casting
Billet Hitter
Billet Shear
Dies & Tools Room
Handing Table
Hydraulic Extrusion Press
Trusted by Leading EPCs, Architects & Fabricators
Read how our precision extrusion tolerances, metallurgical traceability, and on-time dispatches empower solar, architectural, and industrial projects across India.
“Astham delivered over 180 metric tons of custom solar purlins and module mounting rails with zero dimensional variance. Their alloy consistency and dispatch schedule outperformed our previous tier-1 suppliers.”
“For our 34-story commercial tower in BKC, we required custom 6063-T6 mullion sections with stringent deflection criteria. Astham’s in-house die tooling and precision extrusion delivered exactly on-spec profiles.”
“We evaluated three extrusion mills for our lightweight EV battery enclosure sub-frames. Astham passed our destructive weldability and hardness tests on the very first batch. Impeccable QA traceability.”
“Precision T-slot aluminium profiles require razor-sharp tolerances to ensure smooth linear guide movement. Astham has been our exclusive framing partner for 3 years without a single rejection.”
“The anodized surface finish and dimensional stability of Astham profiles have elevated our luxury villa window lines. Their team is proactive with custom die development and technical consulting.”
“Supplying heavy structural extrusions for railway rolling stock requires strict EN and ASTM certification. Astham provided certified mill test reports with every lot and met our tight deadline.”
Frequently Asked Procurement Questions
Essential answers regarding custom die development timelines, minimum order quantities, alloy tempers, and CAD non-disclosure policies.
Ready to Discuss Precision Aluminium Extrusions?
Submit your CAD drawings for 24-hour DFM engineering review or schedule a technical consultation with our tooling specialists.